Explore our high-performance warehousing hardware engineered for maximum durability and seamless system integration.
Building the backbone of modern supply chains through uncompromised manufacturing excellence and technological innovation.
Hangzhou RAB Logistics Co., Ltd. is a professional provider of intelligent warehousing and modern logistics solutions. Built on years of industry experience and continuous technological innovation, RAB Logistics is committed to helping enterprises transform traditional warehouse operations into highly automated, data-driven, and efficient supply chain systems.
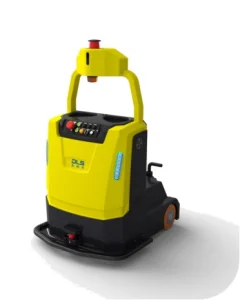
Since its establishment, the company has focused on integrating advanced logistics technologies such as Warehouse Management Systems (WMS), Automated Storage and Retrieval Systems (AS/RS), AGV/AMR robotics, intelligent sorting systems, and real-time data visualization platforms. These solutions enable clients to achieve higher operational accuracy, faster fulfillment speed, and significantly reduced logistics costs.
With strong capabilities in system consulting, solution design, equipment integration, software development, and project implementation, Hangzhou RAB Logistics Co., Ltd. delivers end-to-end intelligent logistics solutions tailored to diverse industry needs. Our expertise ensures seamless coordination between hardware and software, creating scalable and future-ready warehouse infrastructures.
RAB Logistics serves a wide range of industries including manufacturing, cross-border e-commerce, fast-moving consumer goods (FMCG), pharmaceuticals, and automotive parts. Our solutions are trusted for their stability, innovation, and proven performance in complex, high-demand environments.
By choosing Hangzhou RAB Logistics Co., Ltd., you are selecting a long-term strategic partner dedicated to building smarter warehouses, optimizing supply chains, and empowering businesses with sustainable competitive advantages in the era of intelligent logistics.
Navigating the macro shifts in global supply chains, automation demands, and structural shelving requirements.
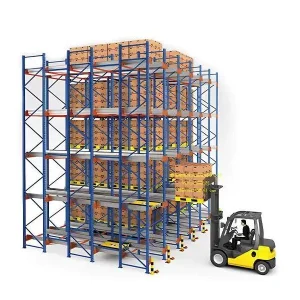
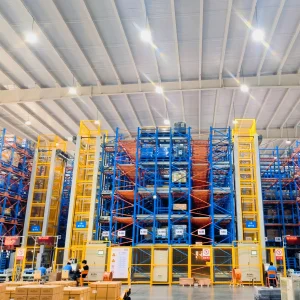
Rapid expansion of global e-commerce and multi-channel fulfillment has accelerated the demand for vertical warehouse optimization. Heavy duty shelving acts as the structural foundation for high-density storage, minimizing footprint while maximizing cubic capacity utilization.
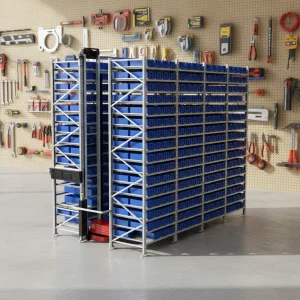
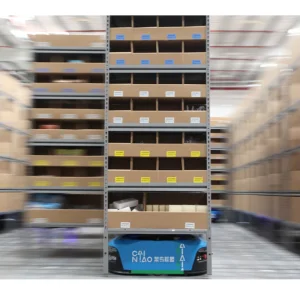
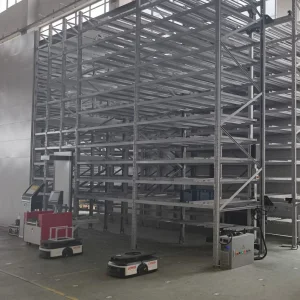
Traditional static shelving is evolving into smart, connected ecosystems. Integration with Automated Storage and Retrieval Systems (AS/RS), automated shuttles, and robotic pickers demands strict load-bearing tolerances and precision manufacturing tolerances.
With international safety standards (FEM, RMI, AS/steel standards) becoming more stringent, global enterprises prioritize certified factories that guarantee structural integrity, seismic resistance, and long-term corrosion protection.
Pioneering smart warehousing technologies to future-proof enterprise supply chain operations.
We leverage high-grade carbon steel, automated cold-roll forming, and embedded RFID/IoT asset tagging. This evolution transforms passive storage structures into active nodes within the warehouse management software (WMS), enabling real-time inventory tracking, predictive maintenance, and weight-load monitoring.
Our production pipelines are optimized for energy efficiency, utilizing eco-friendly powder coating, low-emission welding, and recyclable heavy-duty components. RAB Logistics is dedicated to helping partners achieve green logistics goals without compromising structural load performance.
Ensuring seamless deployment across international borders with rigorous standards and localized engineering backup.
All heavy-duty shelving and structural components are manufactured in strict compliance with ISO9001, CE, RMI, and FEM guidelines, ensuring compatibility with overseas engineering codes.
Tailored engineering designs built for diverse environments—from high-humidity cold storage facilities and seismic-active zones to heavy automotive parts distribution hubs and pharmaceutical cleanrooms.
From initial structural load calculation and CAD/BIM layout design to professional on-site installation supervision and lifetime technical maintenance support worldwide.
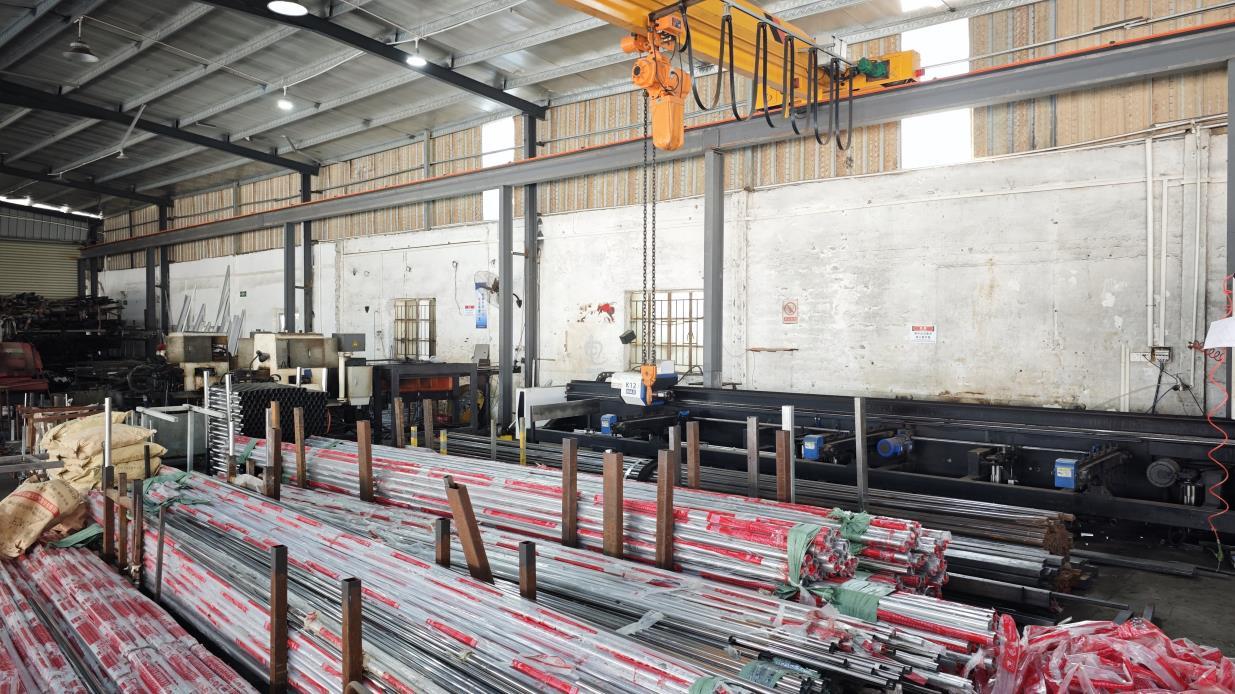
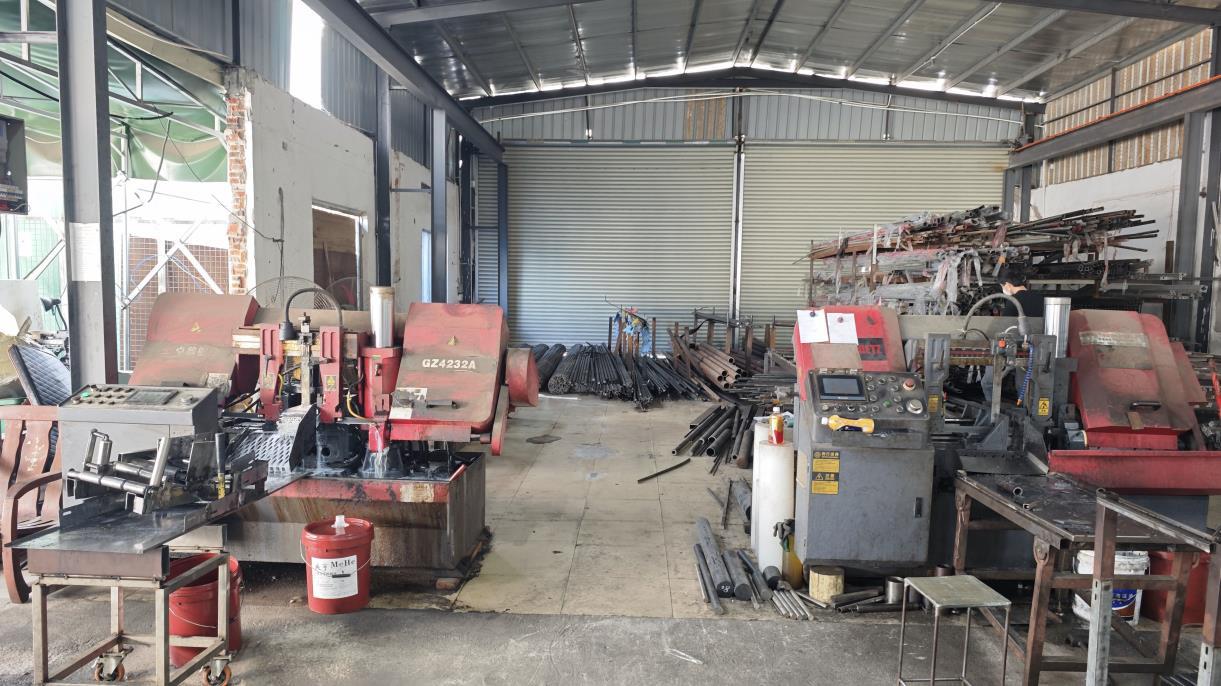
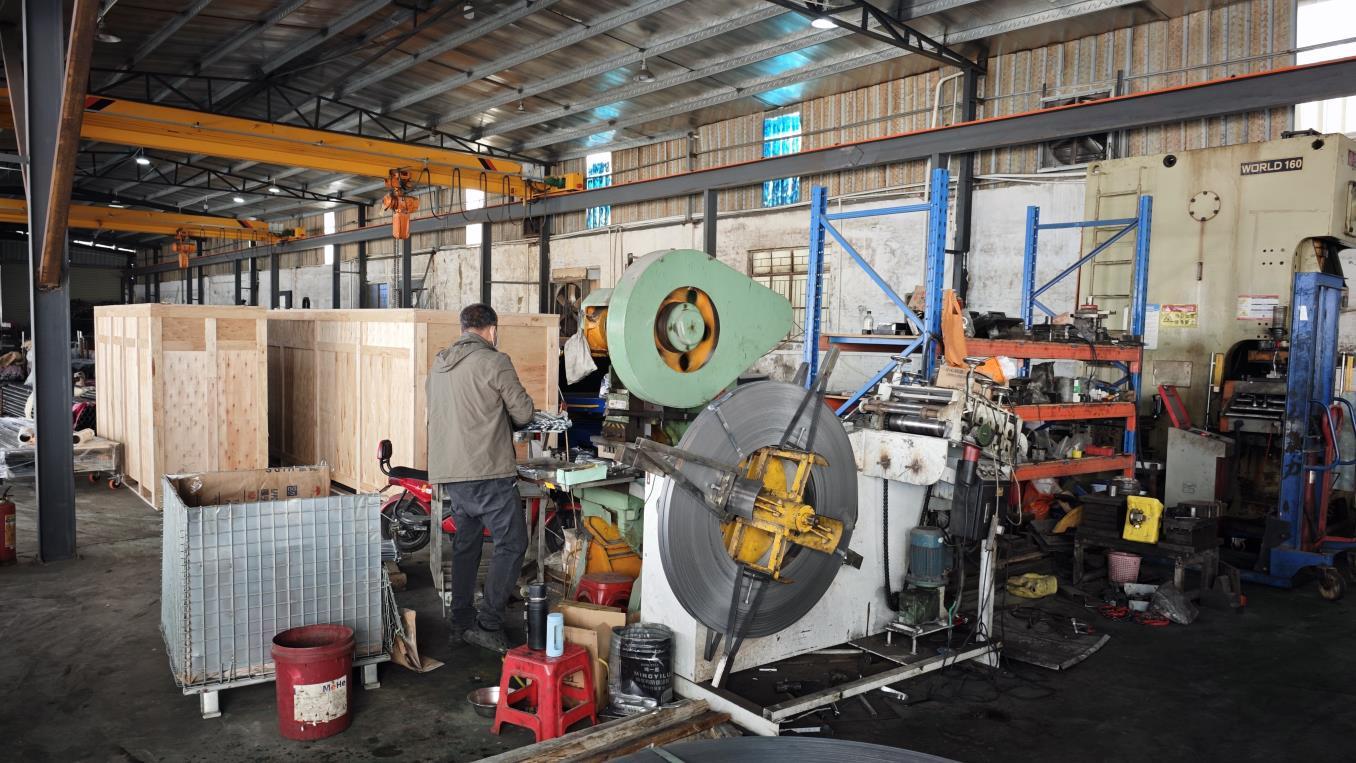
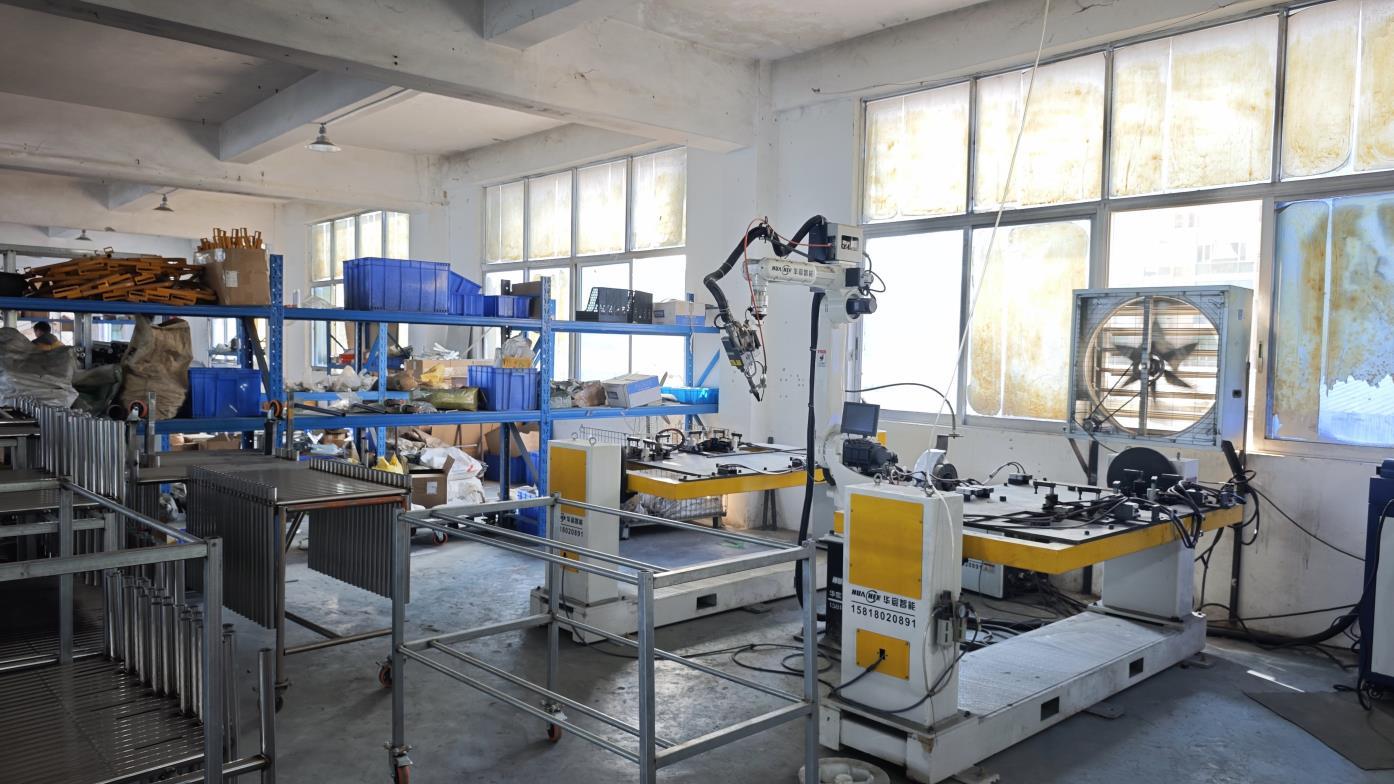
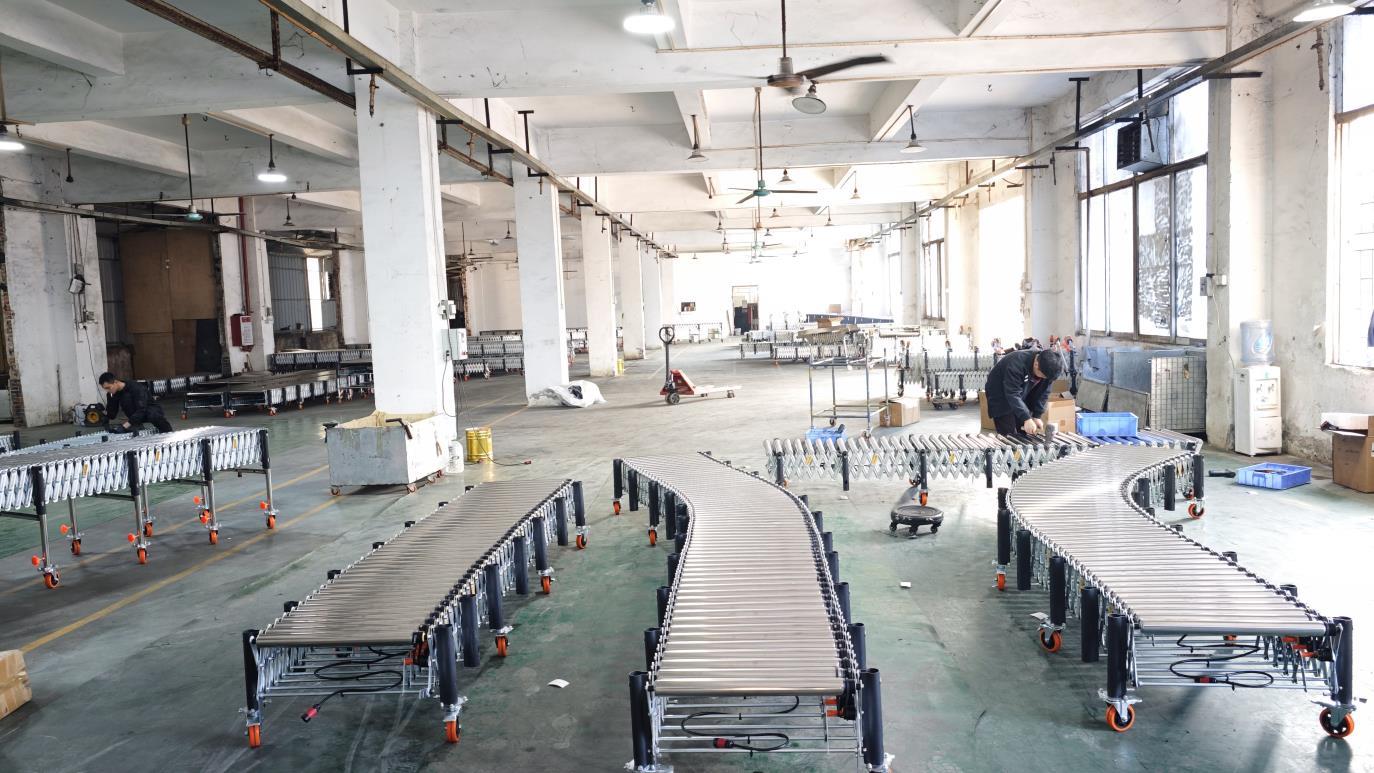
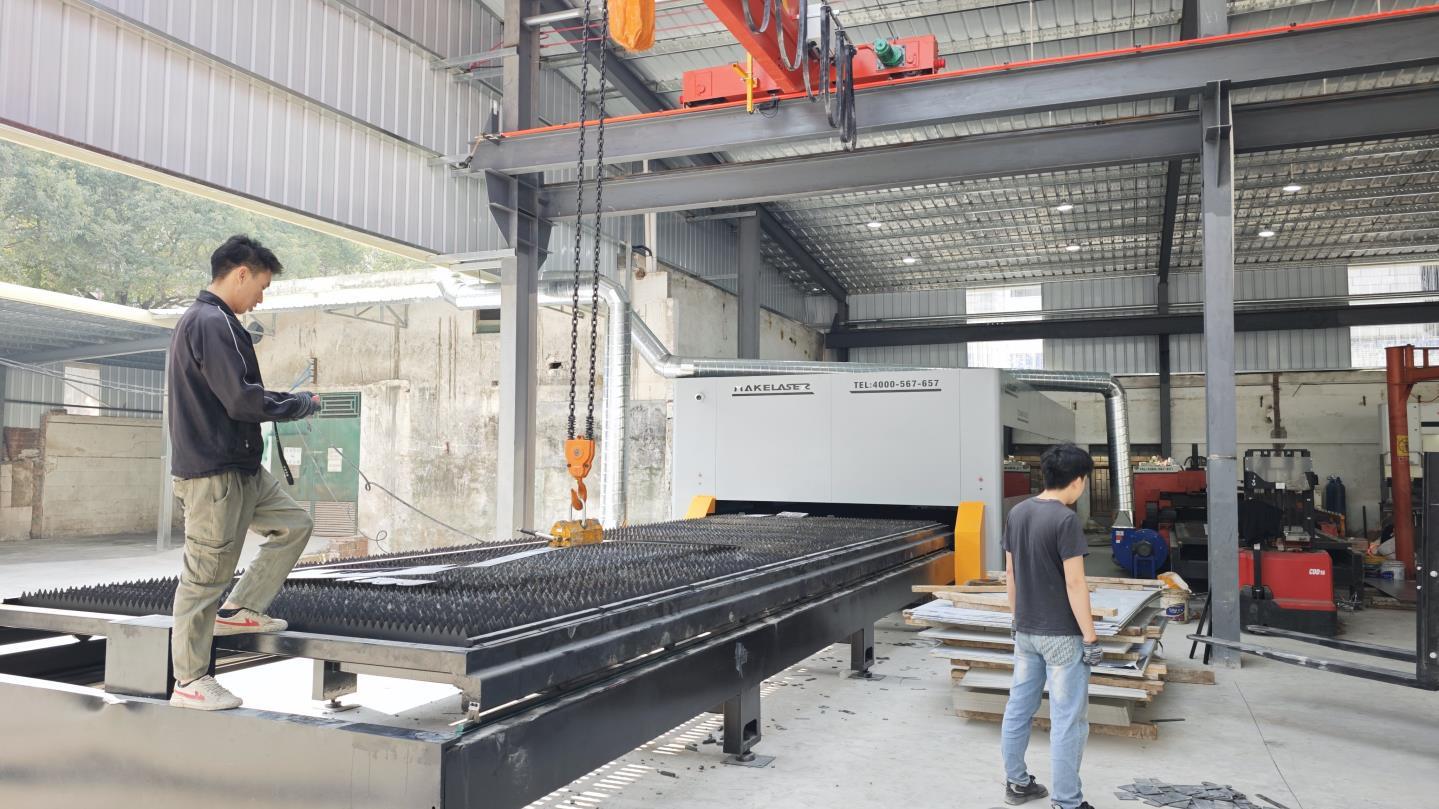
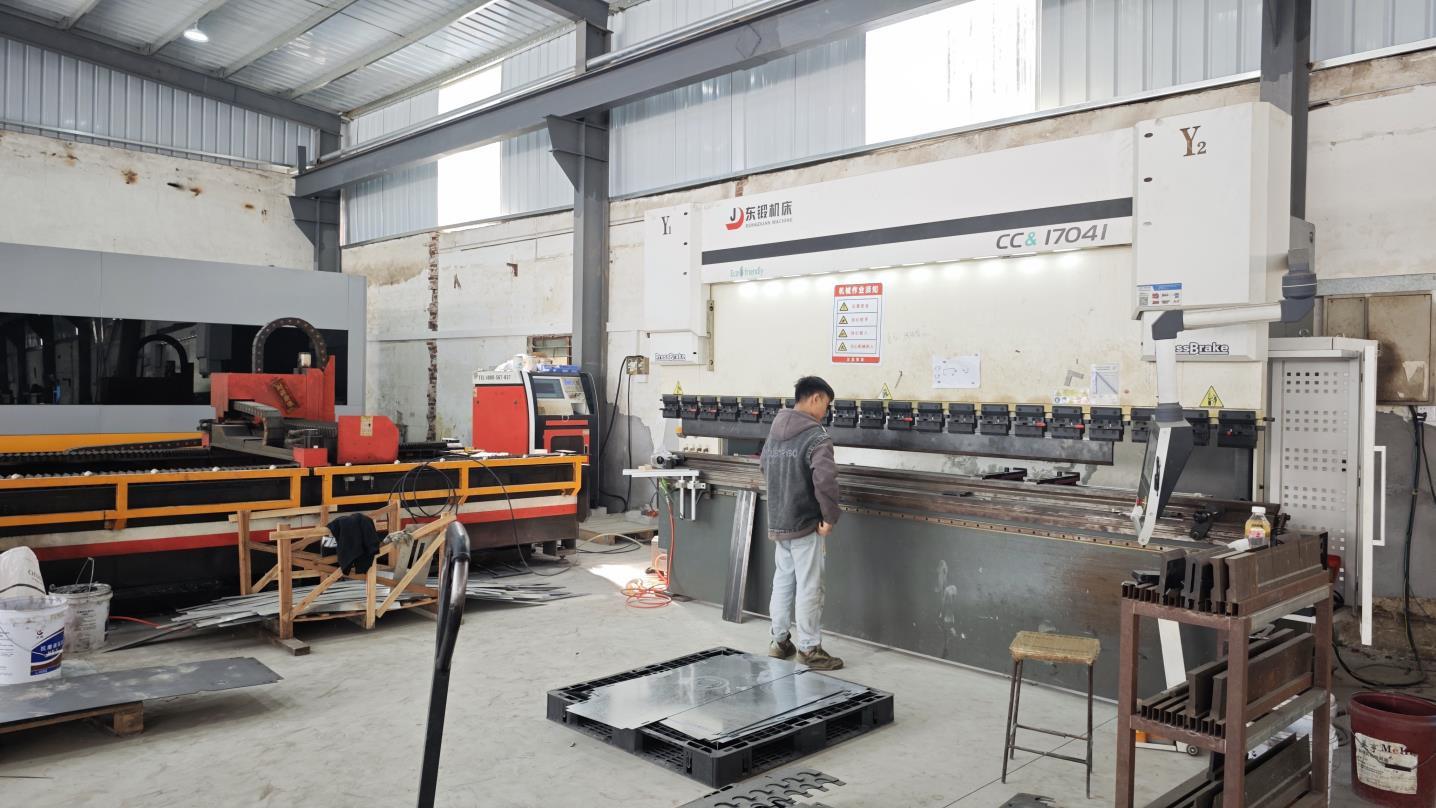
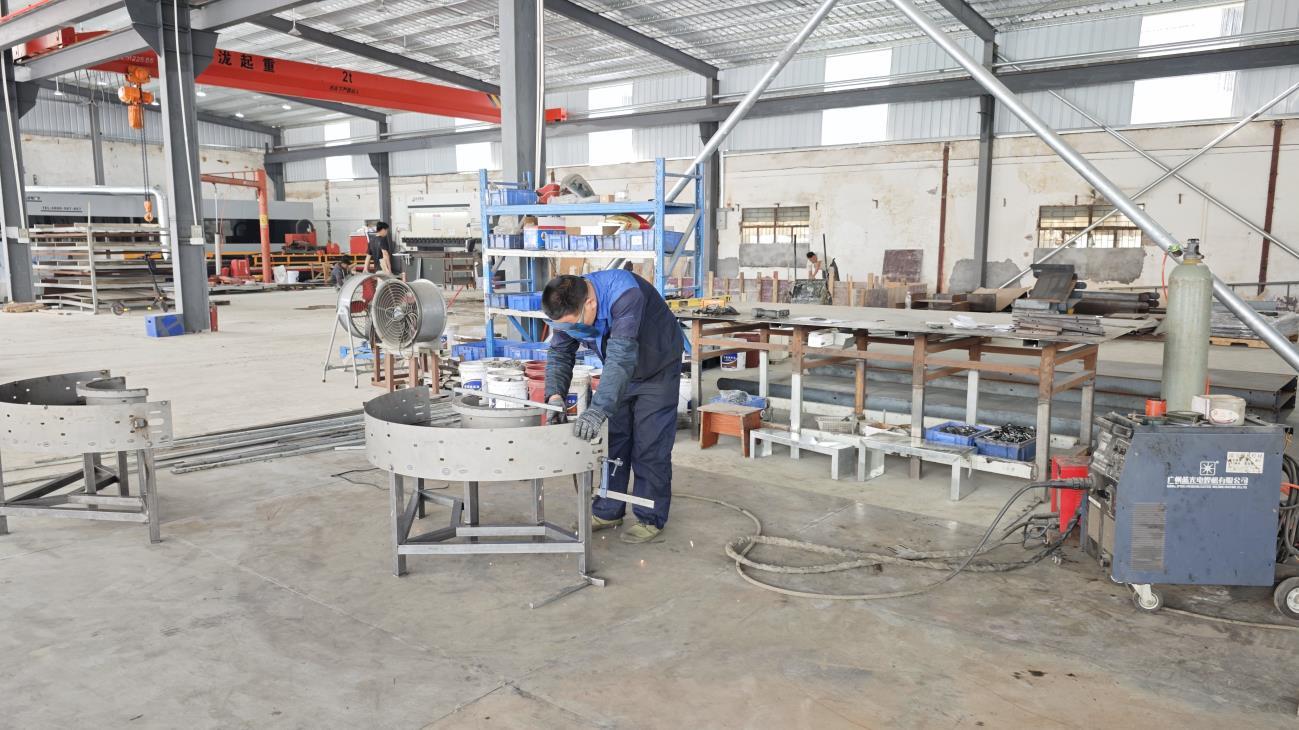
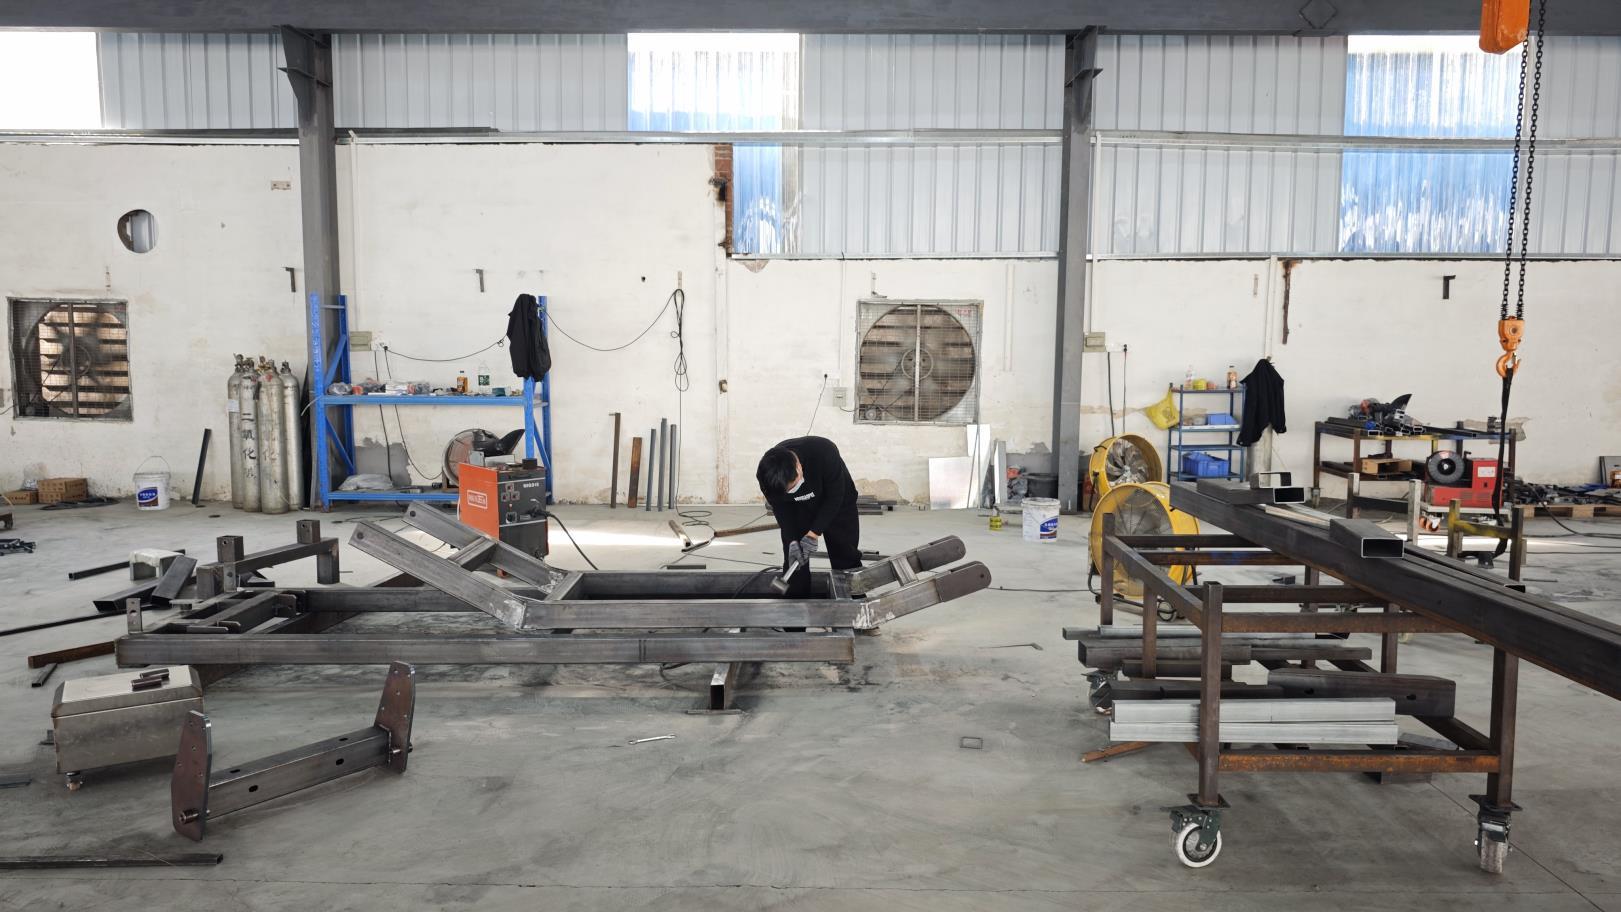
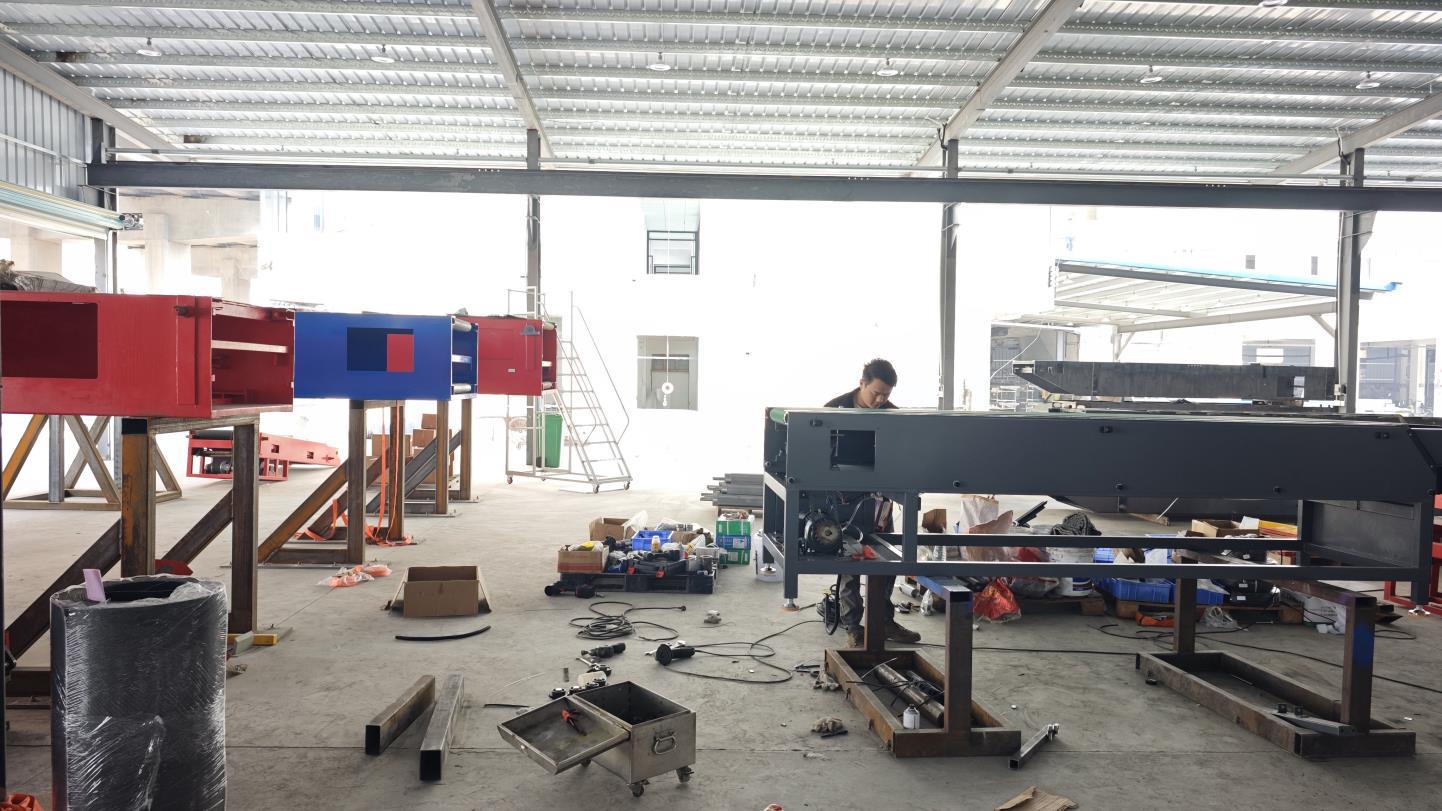
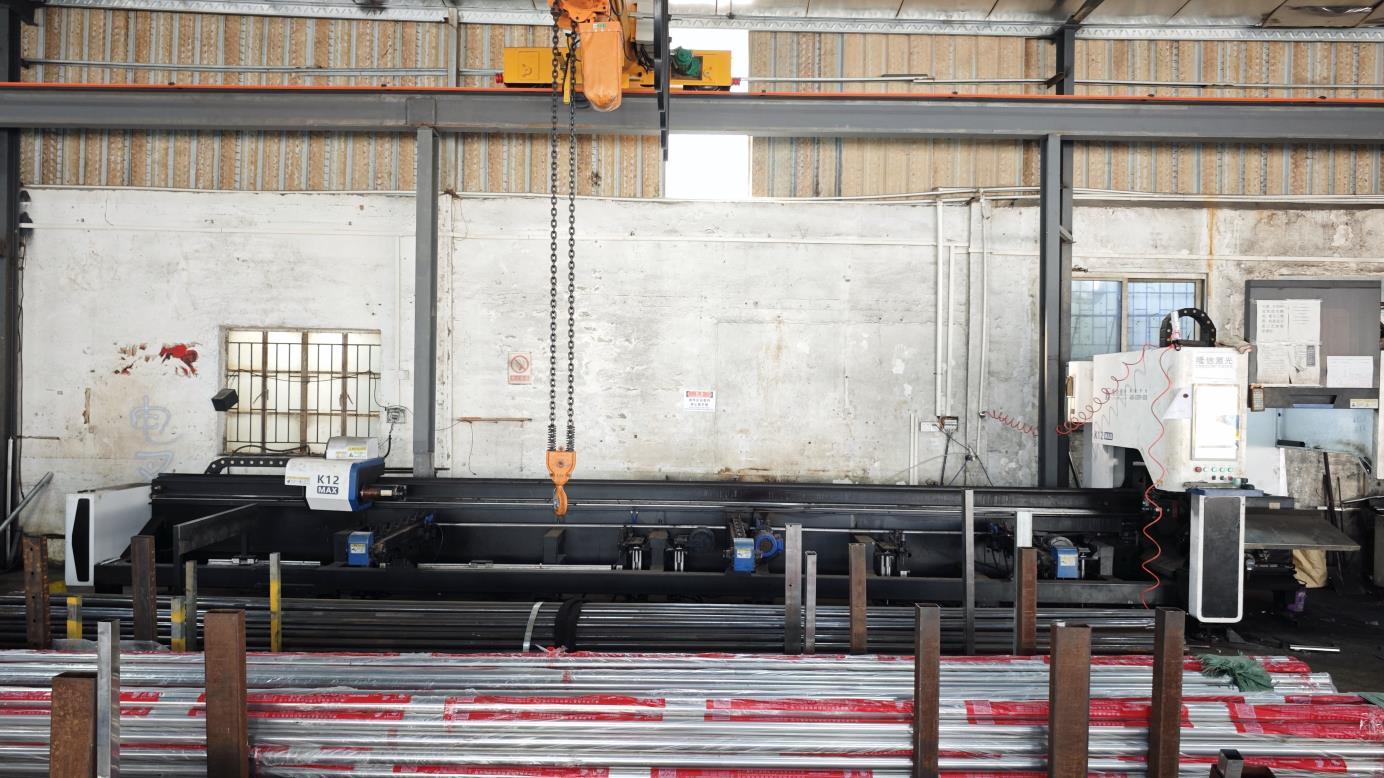
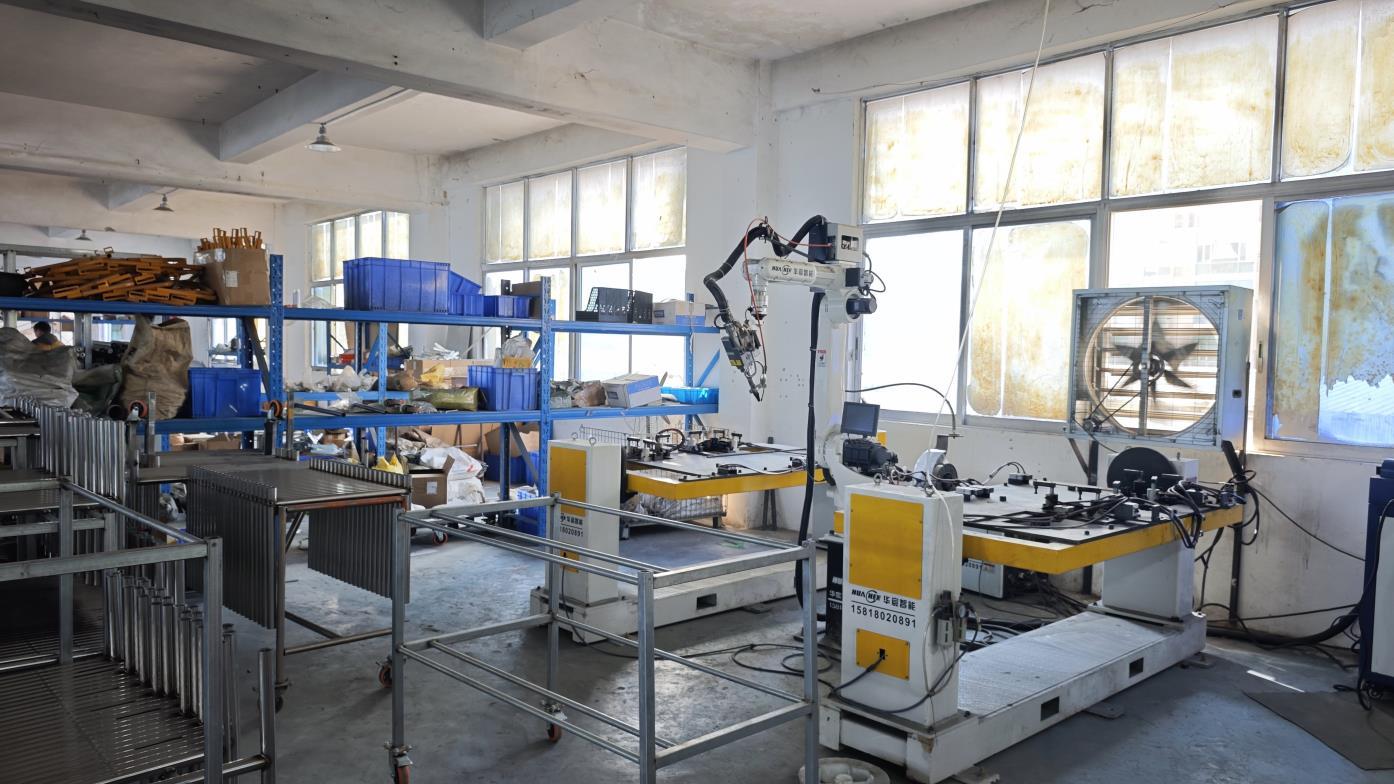
Precision engineering powered by state-of-the-art machinery and rigorous quality control protocols.
Expert answers regarding heavy-duty shelving specification, factory direct sourcing, and automated integration.
Our heavy-duty shelving systems are engineered using high-grade structural carbon steel, precision CNC bending, and robotic welding. They are specifically designed to support high load capacities per tier, resist seismic stress, and integrate smoothly with automated systems like AS/RS and AGVs.
Yes. As a direct manufacturer, we offer full customization services including bespoke height, depth, tier load capacity, and anti-corrosion surface treatments tailored precisely to your architectural blueprint.
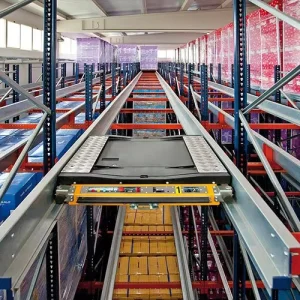
Absolutely. Our intelligent systems, multi-tier shuttle racks, and automated equipment feature open API integration capabilities, ensuring seamless real-time data synchronization with your existing WMS, WCS, or ERP platforms.
Our factory operations adhere strictly to ISO9001 quality management standards, with products complying with international safety standards such as CE, RMI, and FEM guidelines for structural load safety.
Discover our specialized automated machinery, intelligent software, and high-density material handling systems.
 RAB Logistics