Explore our engineered heavy-duty storage, structural solutions, and automated material handling infrastructure.
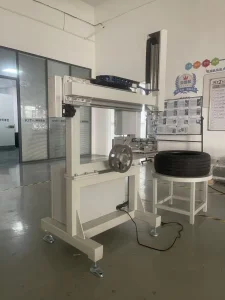
In the fast-evolving landscape of global supply chain management, distribution centers and e-commerce fulfillment hubs face unprecedented pressure regarding throughput velocity and spatial optimization. Carton flow racking, commonly known as gravity flow rack, has emerged as an indispensable cornerstone of modern order fulfillment. By leveraging inclined roller tracks and gravity, cartons automatically slide from the replenishment face to the pick face, executing the First-In, First-Out (FIFO) inventory rotation principle effortlessly.
Across North American, European, and Asia-Pacific markets, enterprises are transitioning from traditional static shelving to high-density dynamic storage. This shift is primarily driven by the explosion of SKU proliferation in sectors such as apparel, pharmaceuticals, cosmetics, and fast-moving consumer goods (FMCG). Modern warehouses can no longer afford the horizontal footprint waste associated with conventional selective pallet racking when picking split cases. Custom OEM carton flow racking solutions bridge this operational gap by maximizing vertical cubic capacity while dramatically reducing picker travel time.
China has established itself as the premier global epicenter for the manufacturing and export of custom OEM carton flow racking systems. This dominance is not merely a function of cost competitiveness, but rather the result of highly sophisticated industrial clusters, advanced automated manufacturing infrastructure, and stringent quality control protocols.
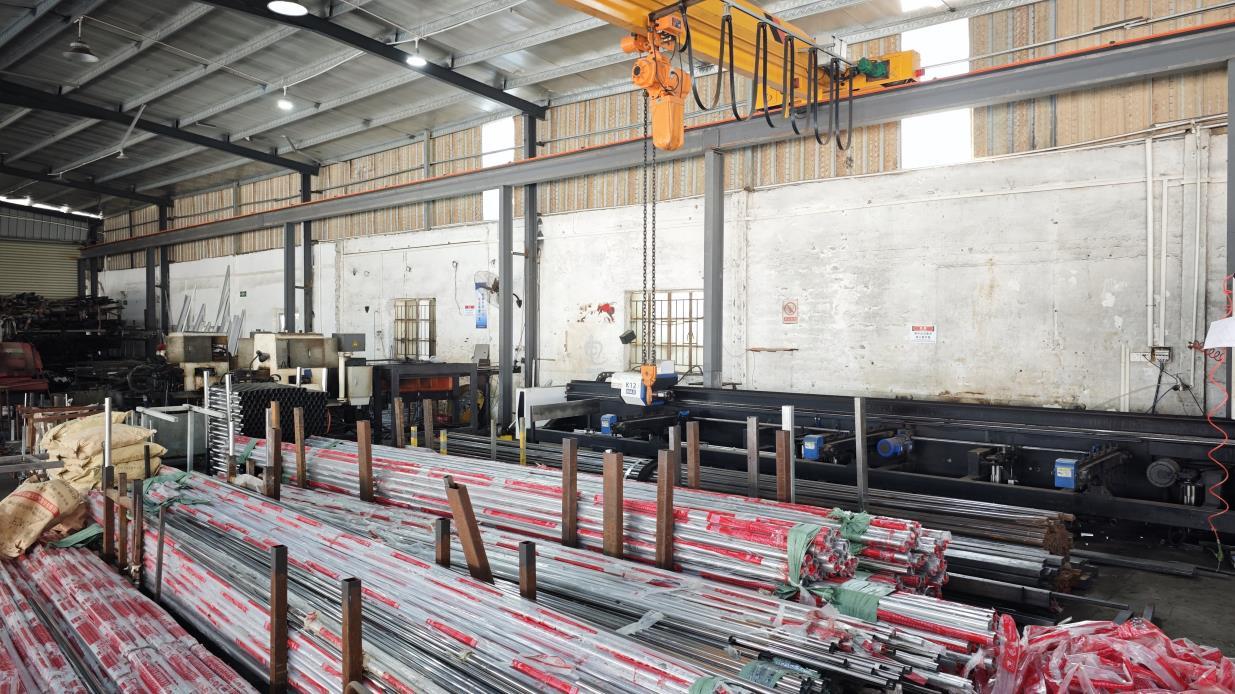
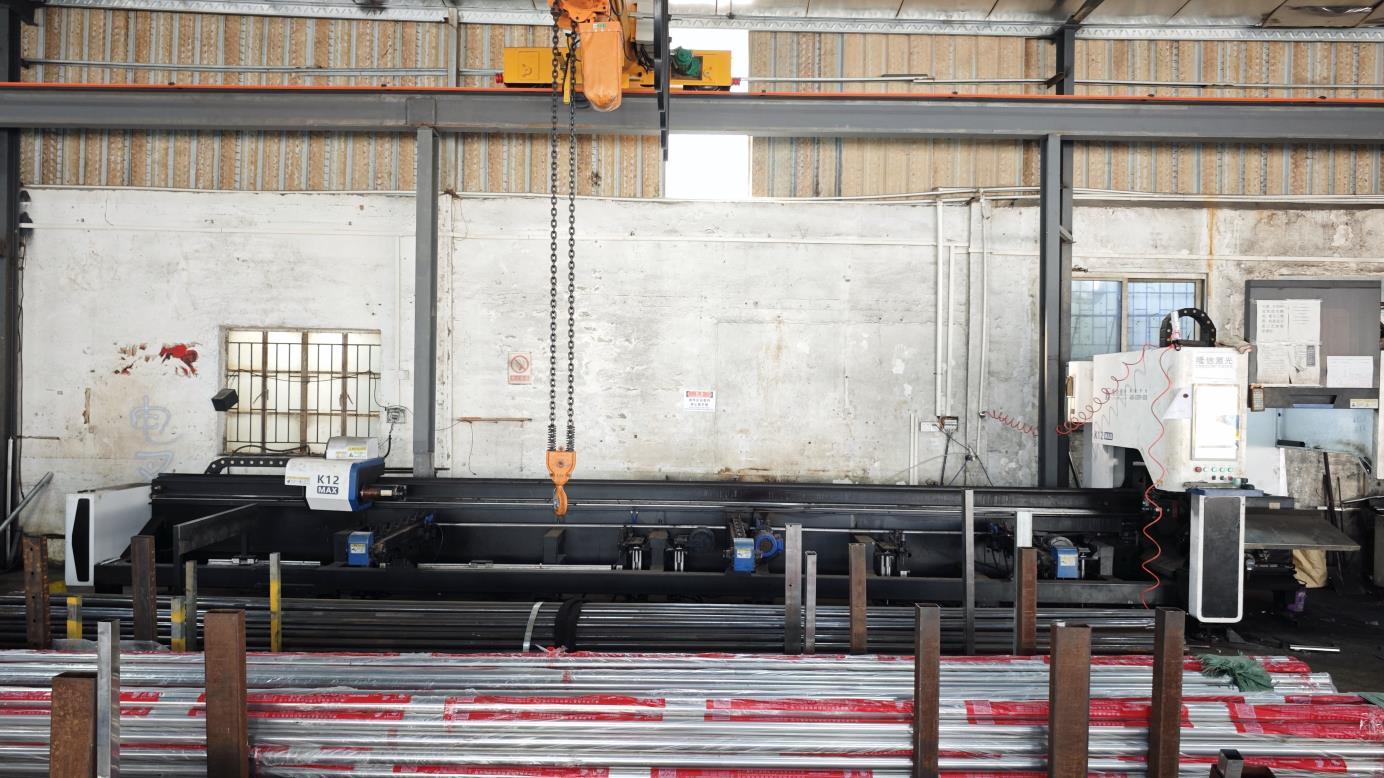
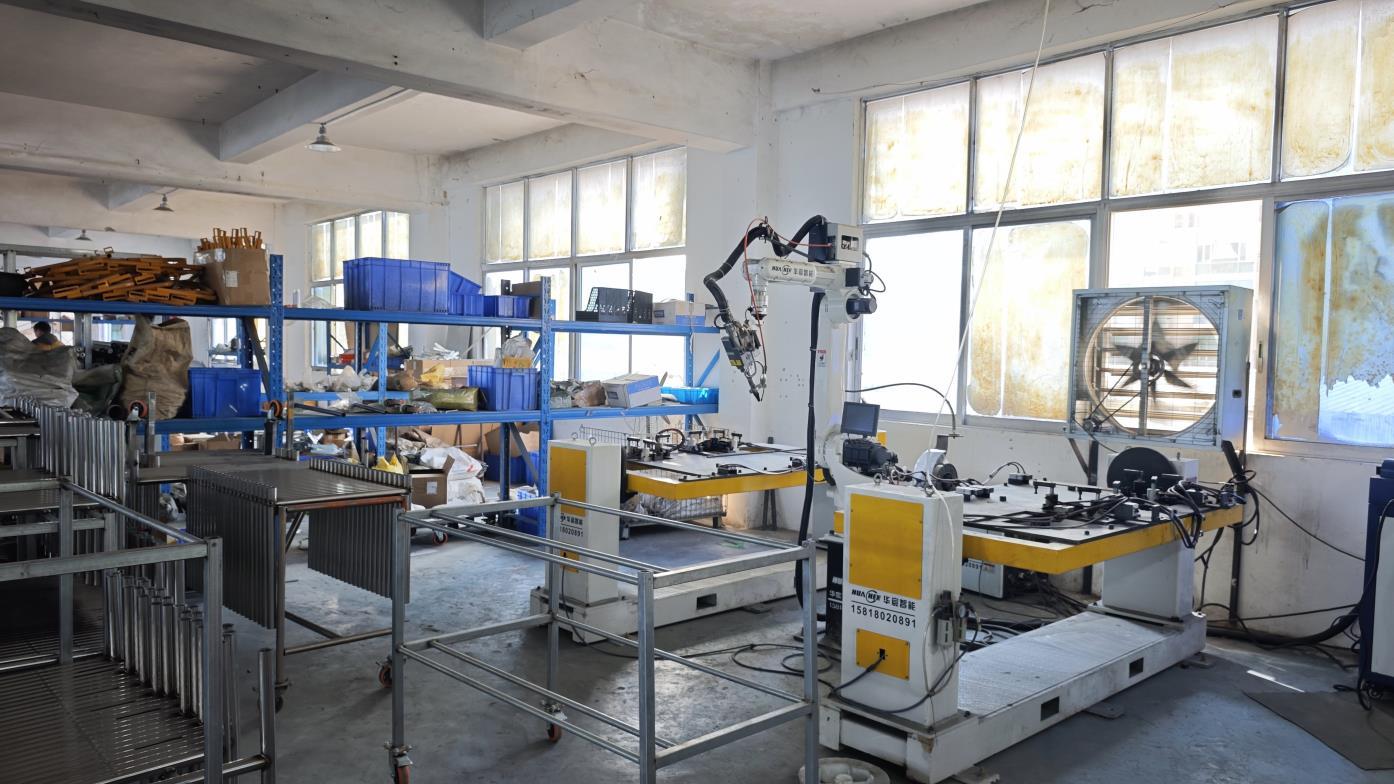
Chinese manufacturing powerhouses utilize state-of-the-art fully automated CNC machinery, precision laser cutting, multi-axis robotic welding, and advanced powder-coating lines to produce structural steel components of uncompromising durability. From heavy-gauge galvanized steel rollers to customizable aluminum track profiles and impact-resistant guide rails, every custom OEM installation is engineered to withstand rigorous, multi-shift industrial environments. Partnering with elite Chinese exporters ensures global businesses receive tailor-made, modular racking systems that comply with international seismic and safety standards (such as RMI, FEM, and AS4084).
Discover complementary intelligent systems designed to streamline warehouse operations and inventory workflows.
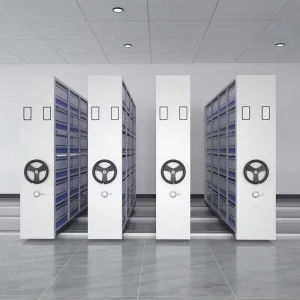
Hangzhou RAB Logistics Co., Ltd. is a professional provider of intelligent warehousing and modern logistics solutions. Built on years of industry experience and continuous technological innovation, RAB Logistics is committed to helping enterprises transform traditional warehouse operations into highly automated, data-driven, and efficient supply chain systems.
Since its establishment, the company has focused on integrating advanced logistics technologies such as Warehouse Management Systems (WMS), Automated Storage and Retrieval Systems (AS/RS), AGV/AMR robotics, intelligent sorting systems, and real-time data visualization platforms. These solutions enable clients to achieve higher operational accuracy, faster fulfillment speed, and significantly reduced logistics costs.
With strong capabilities in system consulting, solution design, equipment integration, software development, and project implementation, Hangzhou RAB Logistics Co., Ltd. delivers end-to-end intelligent logistics solutions tailored to diverse industry needs. Our expertise ensures seamless coordination between hardware and software, creating scalable and future-ready warehouse infrastructures.
RAB Logistics serves a wide range of industries including manufacturing, cross-border e-commerce, fast-moving consumer goods (FMCG), pharmaceuticals, and automotive parts. Our solutions are trusted for their stability, innovation, and proven performance in complex, high-demand environments.
By choosing Hangzhou RAB Logistics Co., Ltd., you are selecting a long-term strategic partner dedicated to building smarter warehouses, optimizing supply chains, and empowering businesses with sustainable competitive advantages in the era of intelligent logistics.
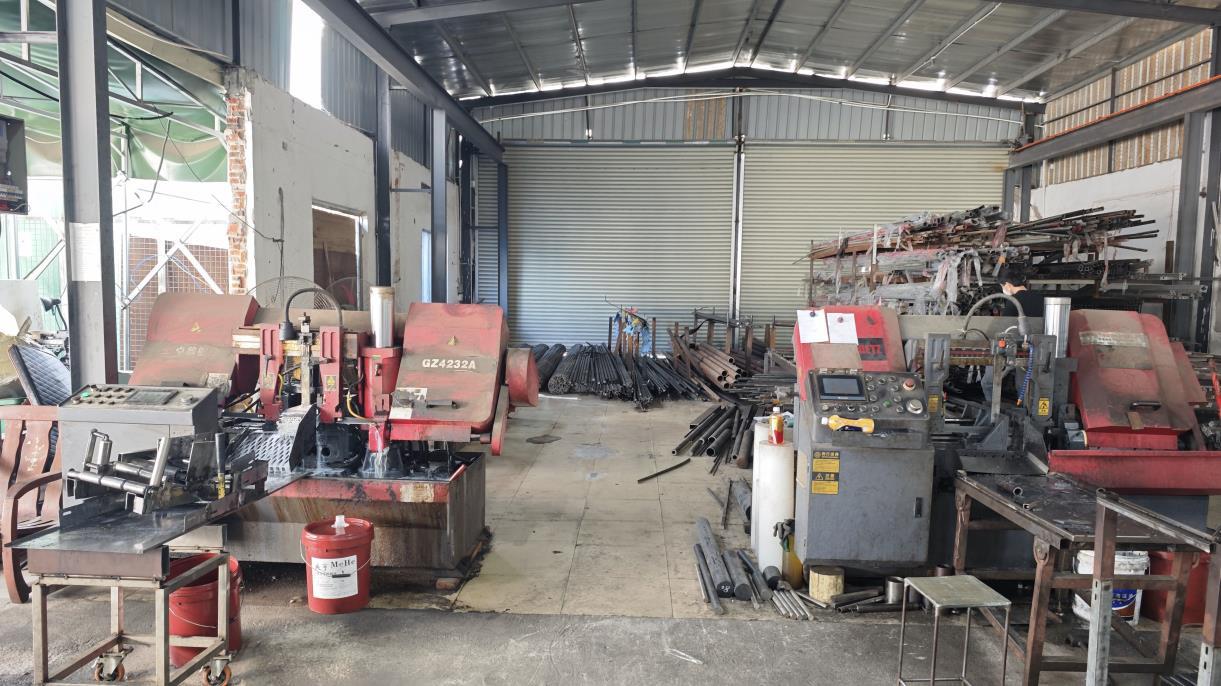
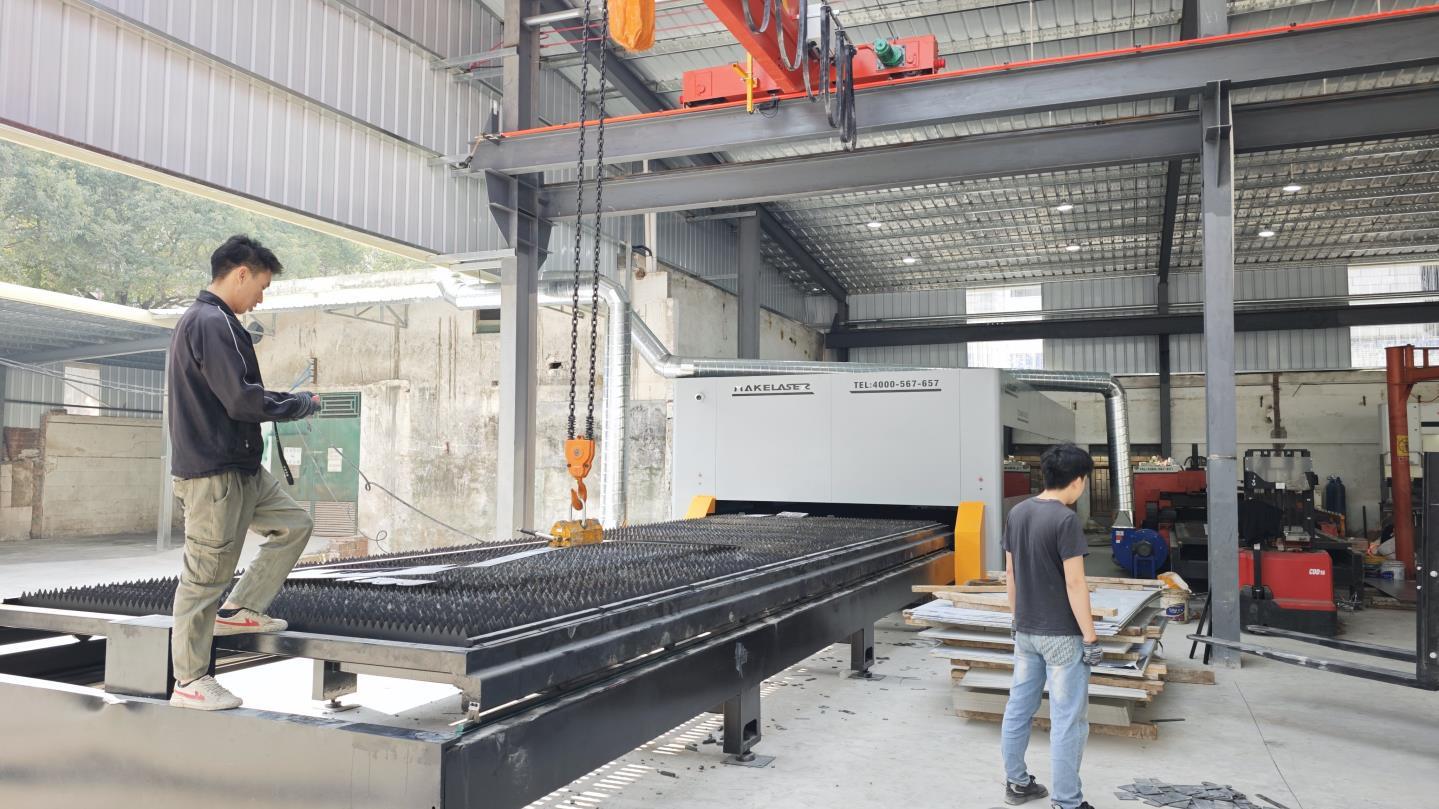
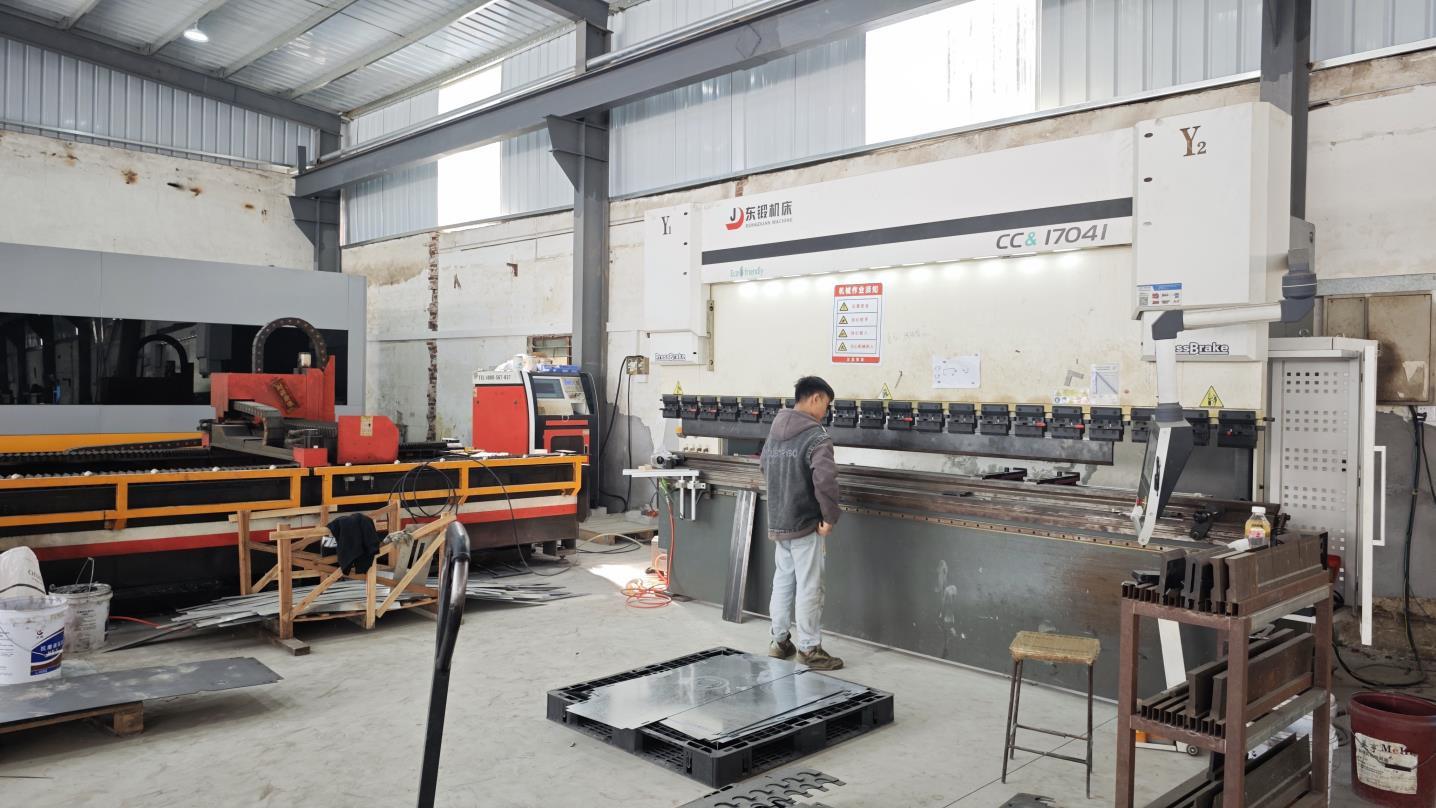
Utilizing fully automatic CNC sawing and cutting machines to achieve millimeter-level precision on raw steel profiles, ensuring structural integrity.
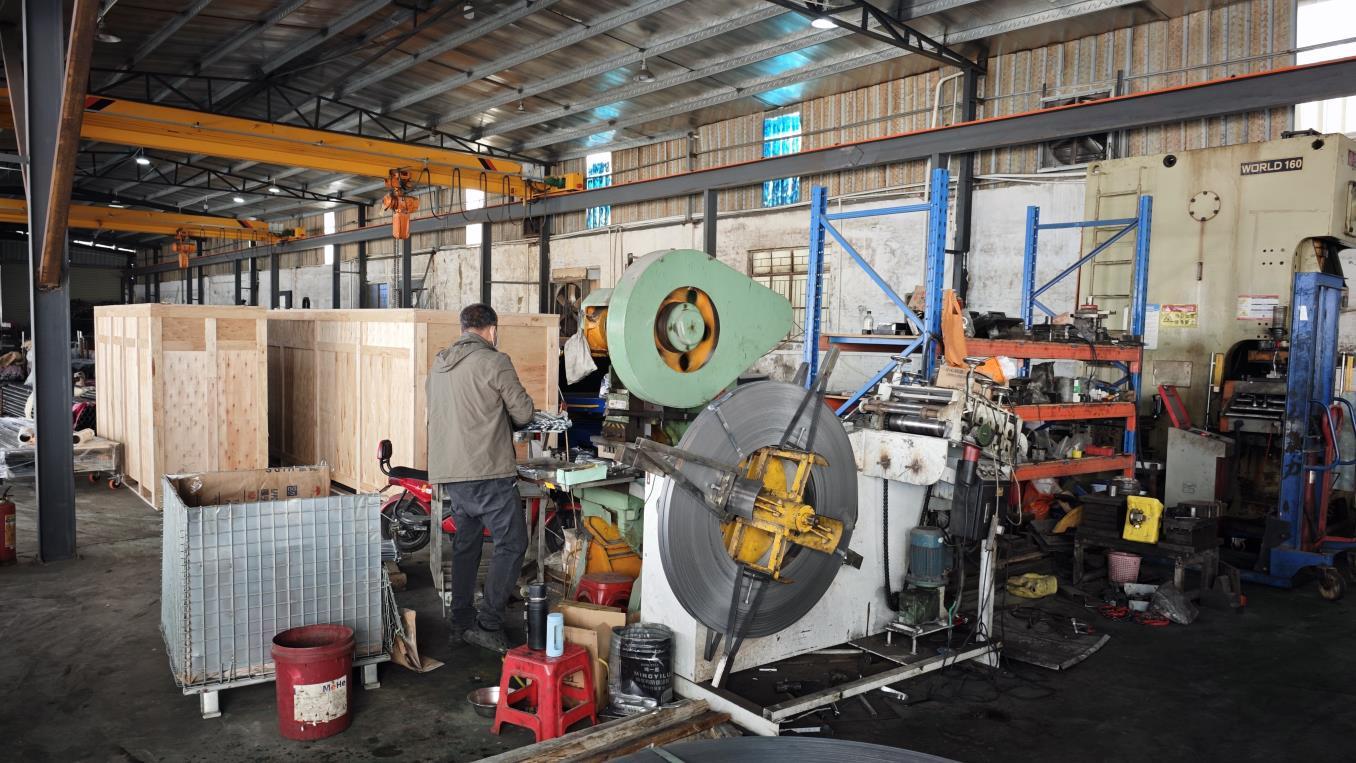
High-tonnage hydraulic presses and press brakes shape connectors, brackets, and upright channels with exact dimensional repeatability.
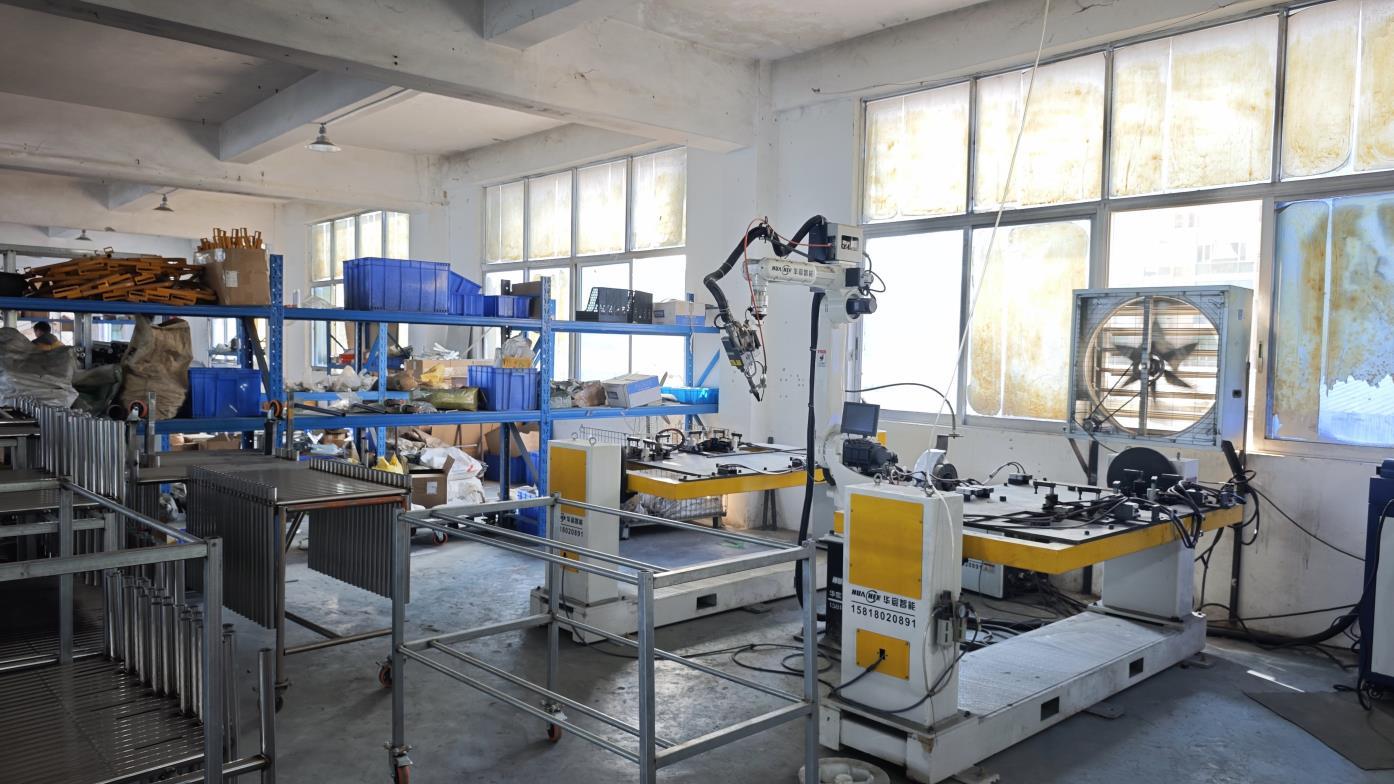
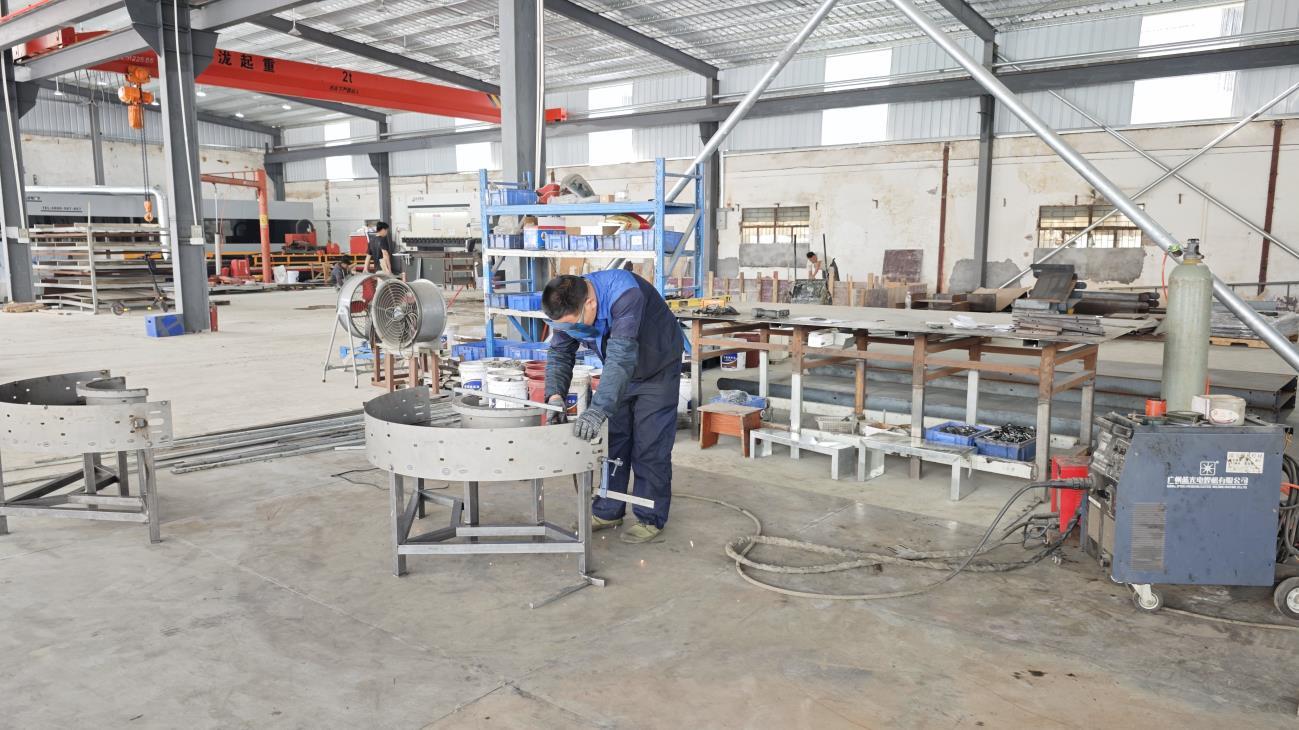
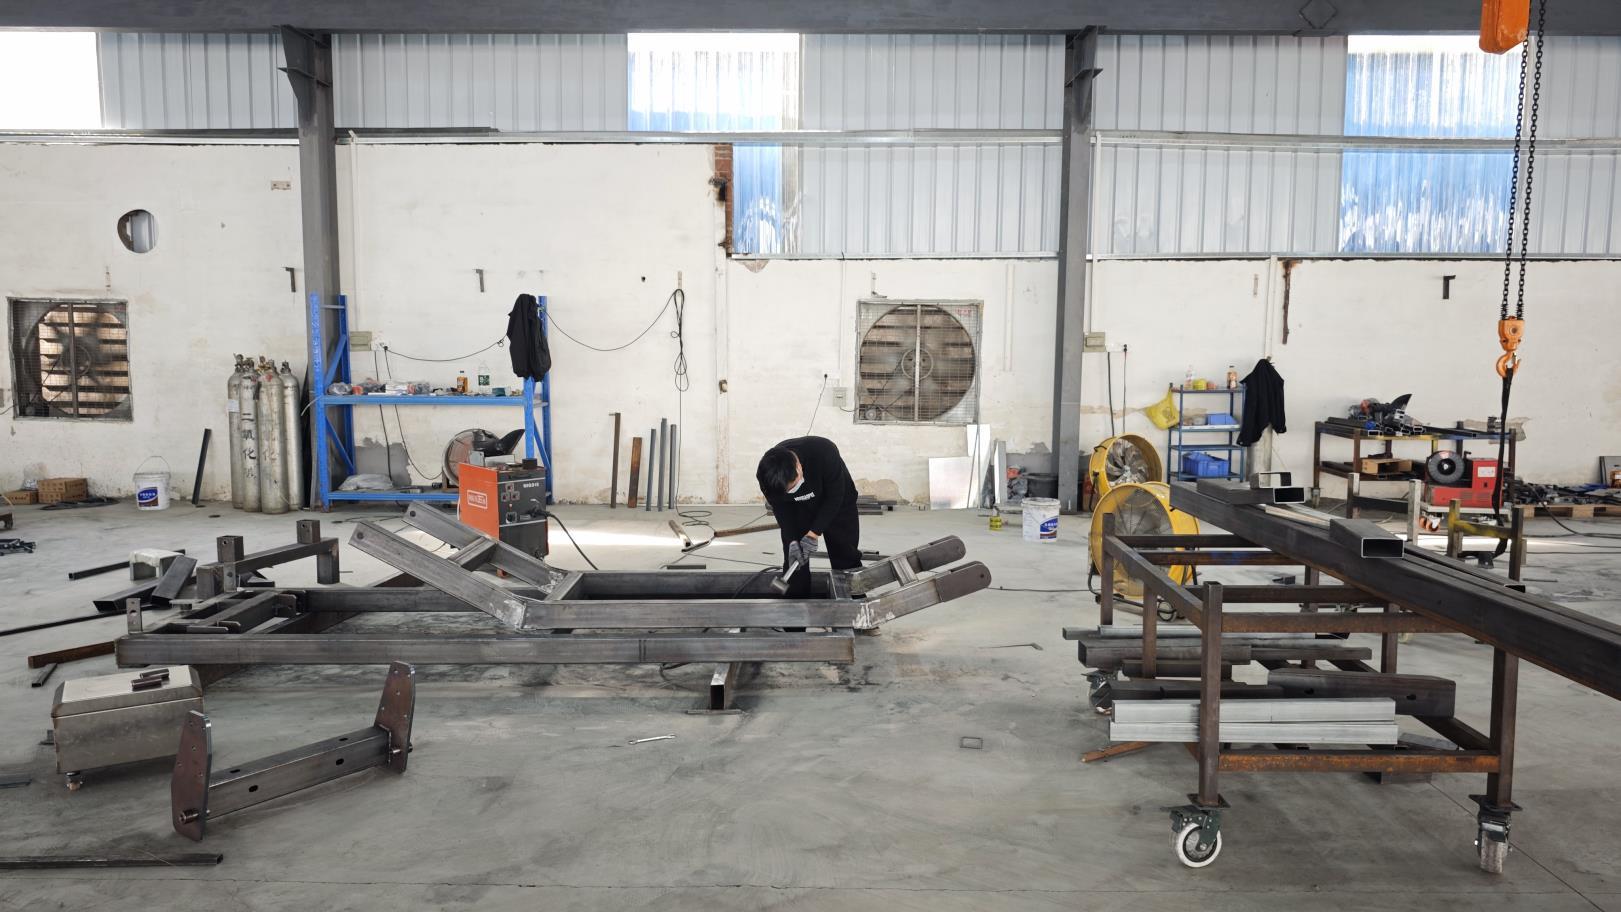
Advanced robotic welding and machine hand spot welders deliver robust, seamless joints capable of sustaining heavy cyclical dynamic loads.
Meticulous surface polishing removes burrs and imperfections, preparing metal substrates for corrosion-resistant electrostatic powder coating.
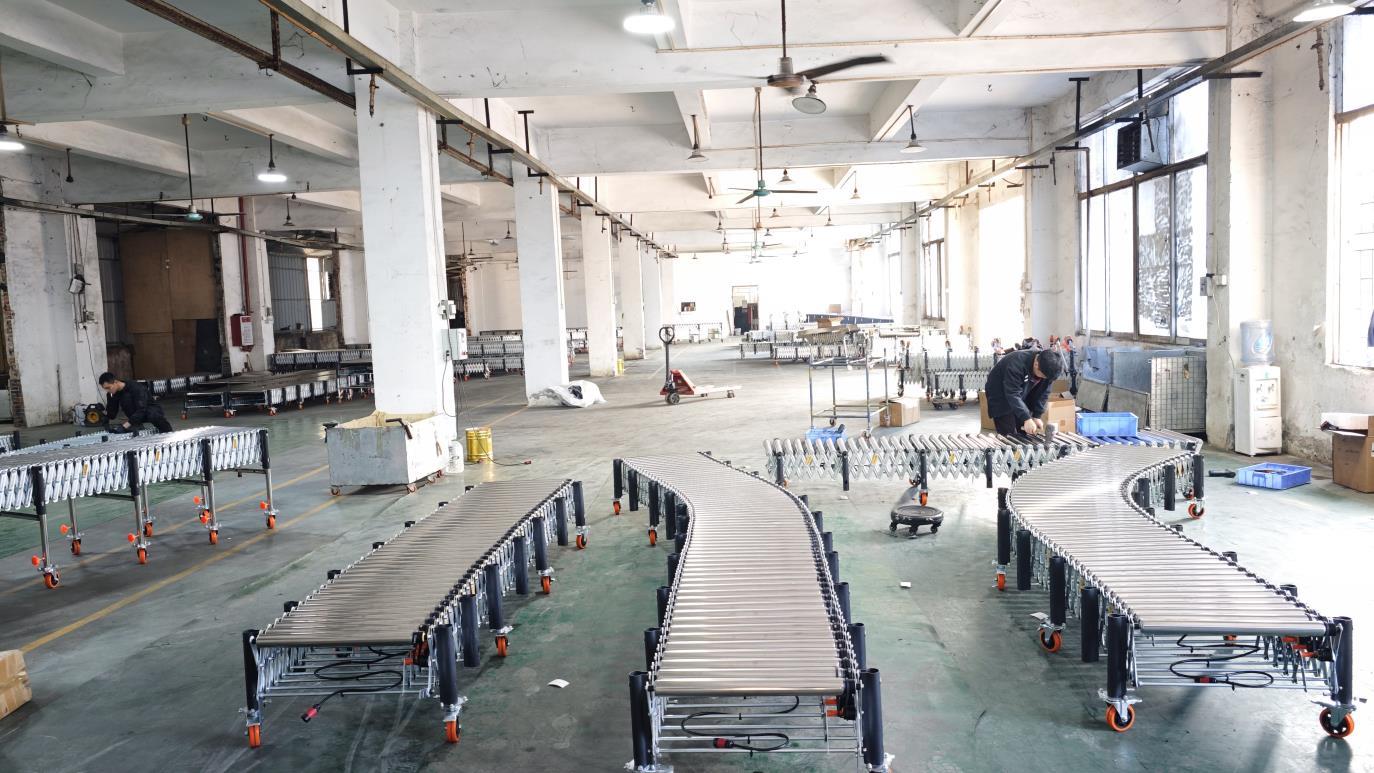
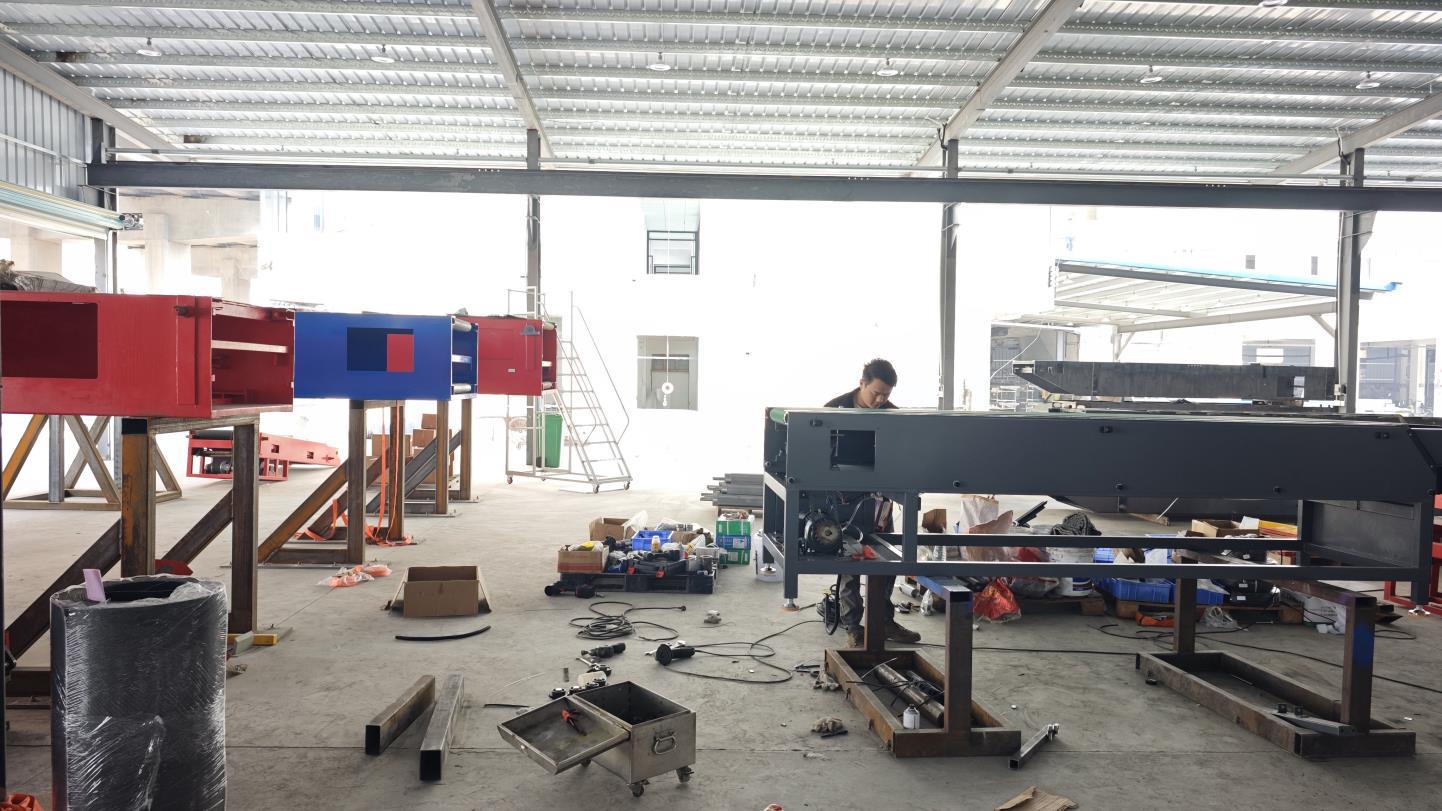
Rigorous pre-assembly trials and inspection protocols guarantee that every custom OEM carton flow module fits together flawlessly on-site.
Engineered to interface seamlessly with pick-to-light systems, conveyor lines, and autonomous mobile robots for ultimate operational synergy.
The convergence of IoT sensors, AI-driven inventory forecasting, and modular gravity racking is redefining the boundaries of warehouse efficiency. Future-proof distribution centers are increasingly adopting "Pick-to-Light" integrated carton flow lanes, where LED displays guide operators instantly to pick locations, slashing error rates to near zero. Furthermore, automated replenishment robotics (AGVs/AMRs) are being paired with flow racks to handle nocturnal restocking, ensuring dawn-to-dusk seamless operational continuity.
Global procurement directors are prioritizing suppliers that offer modular, reconfigurable OEM systems capable of adapting to fluctuating seasonal inventory profiles. Sustainability is another critical pillar; energy-efficient manufacturing processes, recyclable steel materials, and zero-waste packaging are becoming decisive criteria for multinational enterprises sourcing storage hardware from China.
 RAB Logistics