Explore our premier selection of CE certified industrial conveyors, automated storage retrieval systems, and heavy-duty smart material handling equipment designed for maximum operational efficiency.
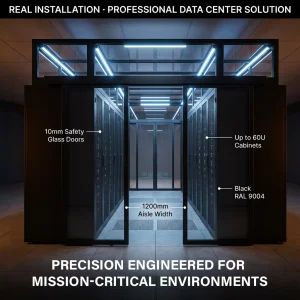
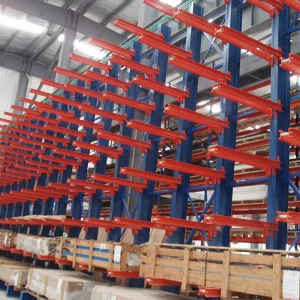
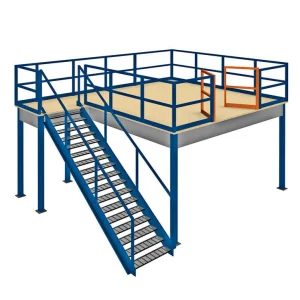
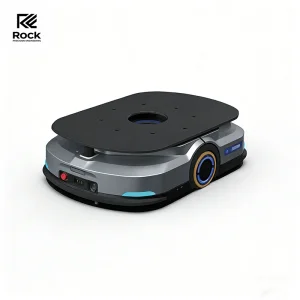
As a leading CE Certified Industrial Conveyors Supplier & Exporters, Hangzhou RAB Logistics Co., Ltd. stands at the forefront of modern supply chain transformation. The global industrial automation landscape is experiencing unprecedented growth, driven by Industry 4.0 paradigms, rapid advancements in robotics, and the unyielding demand for high-speed e-commerce fulfillment. Industrial conveyors no longer merely serve as passive mechanical transit lines; they have evolved into smart neural pathways embedded with IoT sensors, real-time diagnostic algorithms, and adaptive routing logic.
Modern manufacturing facilities, automated distribution centers, and cross-border fulfillment hubs require robust, highly reliable conveying networks capable of operating under harsh, continuous-duty cycles. By integrating precision engineering with state-of-the-art software systems such as WMS, WCS, and MES, our industrial conveyor solutions eliminate bottlenecks, minimize manual intervention, and establish a continuous, data-driven flow of materials from receiving docks to dispatch bays.
Hangzhou RAB Logistics Co., Ltd. is a professional provider of intelligent warehousing and modern logistics solutions. Built on years of industry experience and continuous technological innovation, RAB Logistics is committed to helping enterprises transform traditional warehouse operations into highly automated, data-driven, and efficient supply chain systems.
Since its establishment, the company has focused on integrating advanced logistics technologies such as Warehouse Management Systems (WMS), Automated Storage and Retrieval Systems (AS/RS), AGV/AMR robotics, intelligent sorting systems, and real-time data visualization platforms. These solutions enable clients to achieve higher operational accuracy, faster fulfillment speed, and significantly reduced logistics costs.
With strong capabilities in system consulting, solution design, equipment integration, software development, and project implementation, Hangzhou RAB Logistics Co., Ltd. delivers end-to-end intelligent logistics solutions tailored to diverse industry needs. Our expertise ensures seamless coordination between hardware and software, creating scalable and future-ready warehouse infrastructures.
RAB Logistics serves a wide range of industries including manufacturing, cross-border e-commerce, fast-moving consumer goods (FMCG), pharmaceuticals, and automotive parts. Our solutions are trusted for their stability, innovation, and proven performance in complex, high-demand environments.
By choosing Hangzhou RAB Logistics Co., Ltd., you are selecting a long-term strategic partner dedicated to building smarter warehouses, optimizing supply chains, and empowering businesses with sustainable competitive advantages in the era of intelligent logistics.
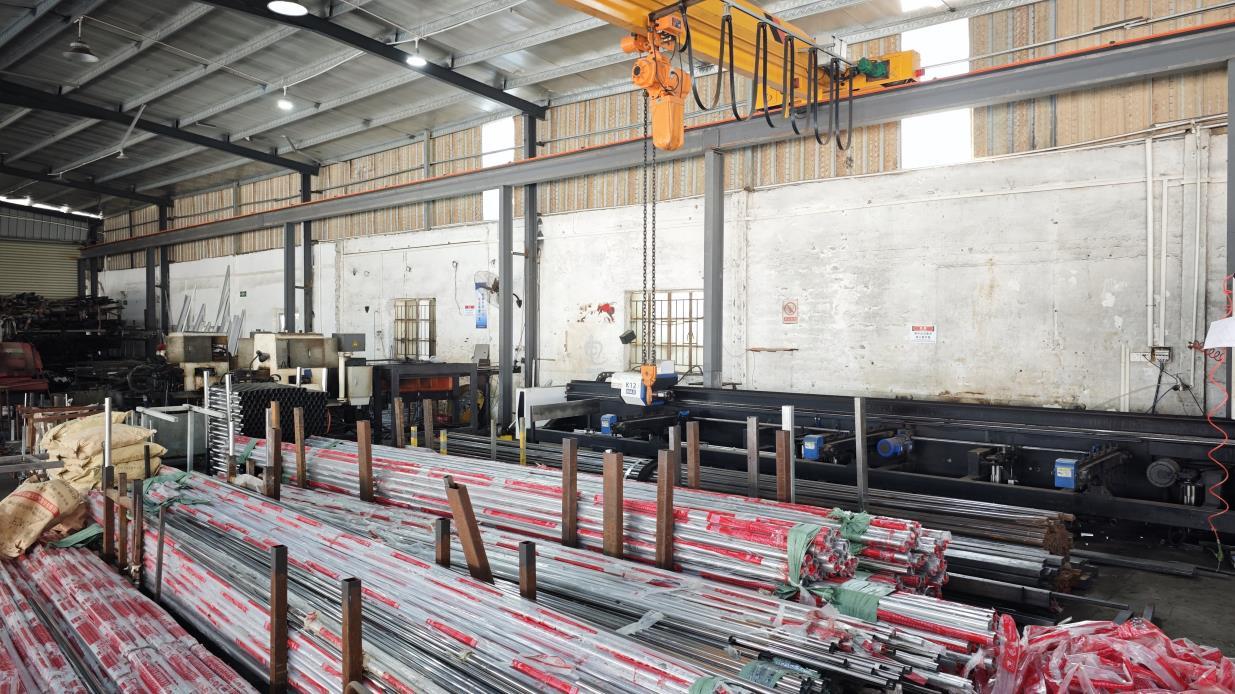
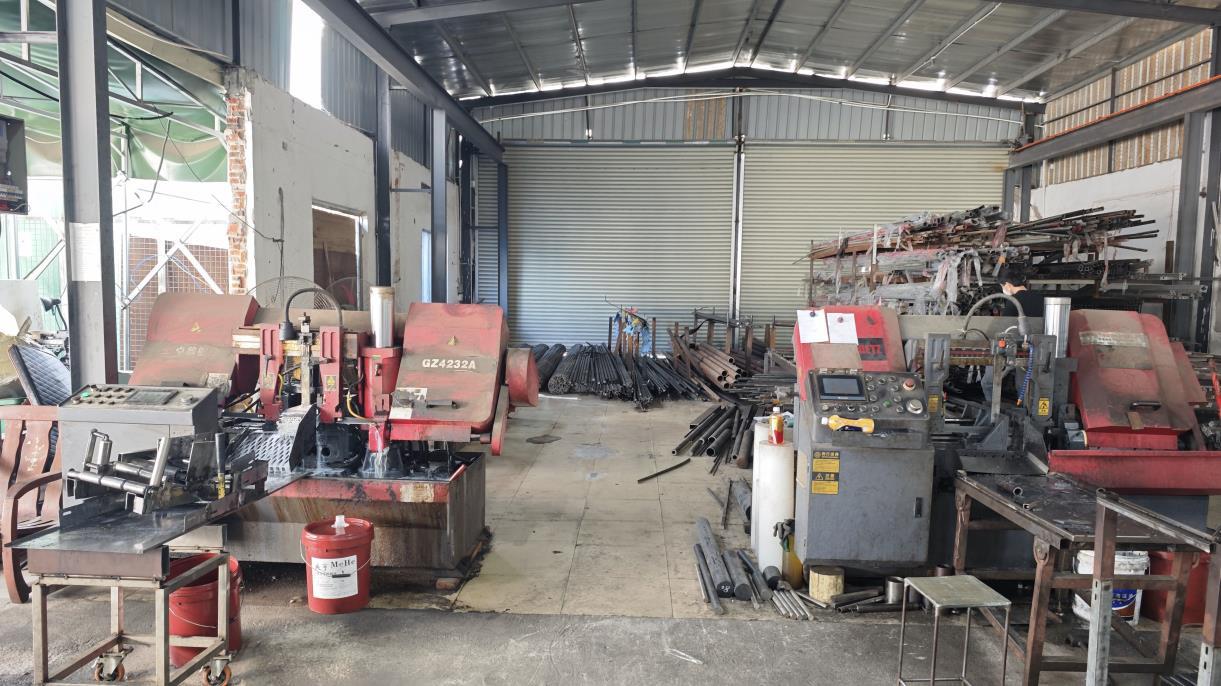
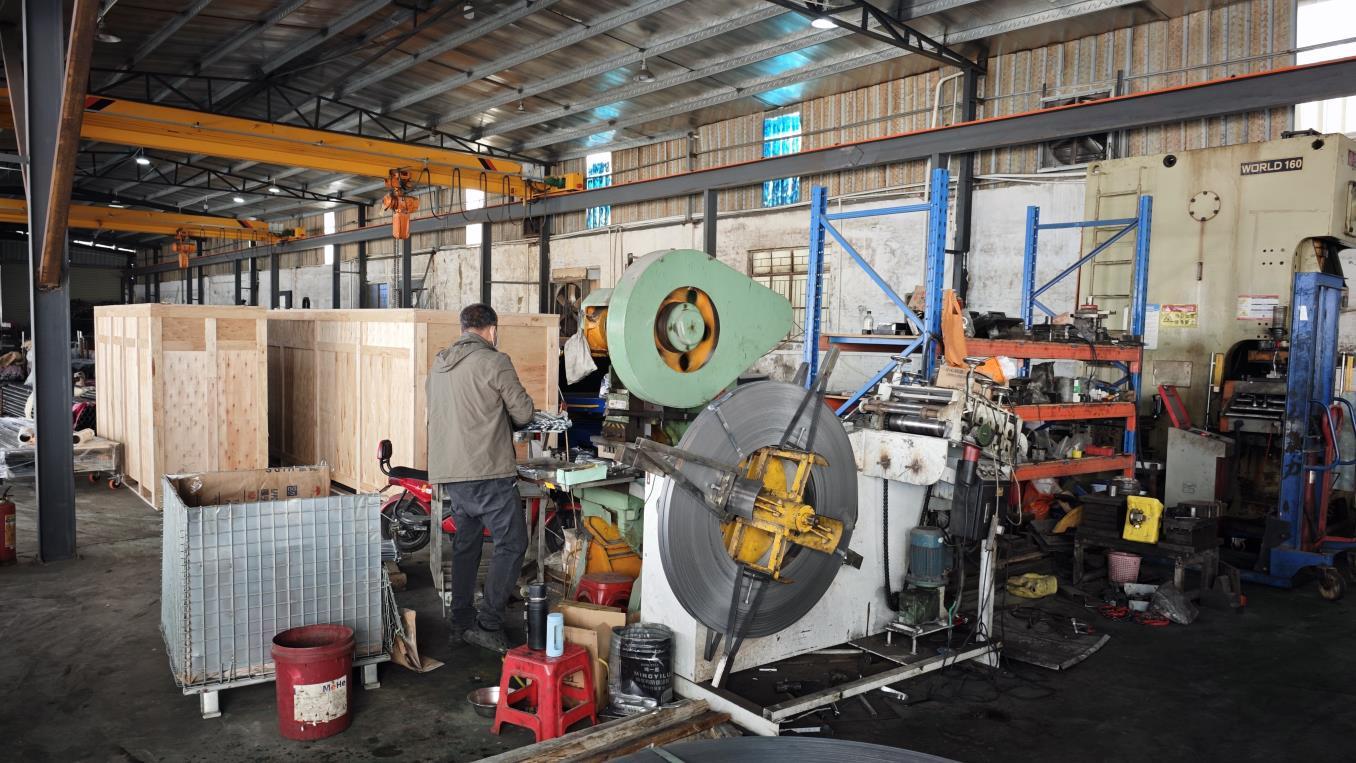
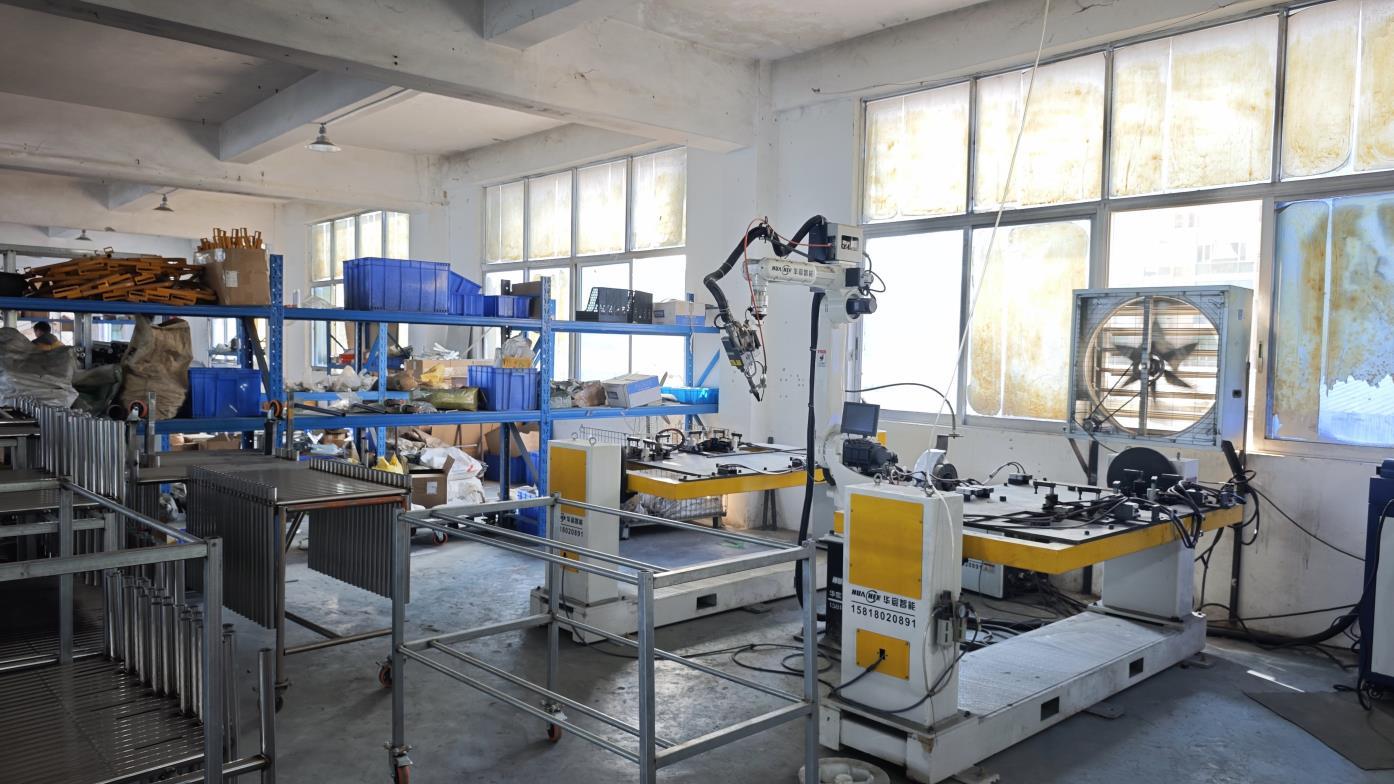
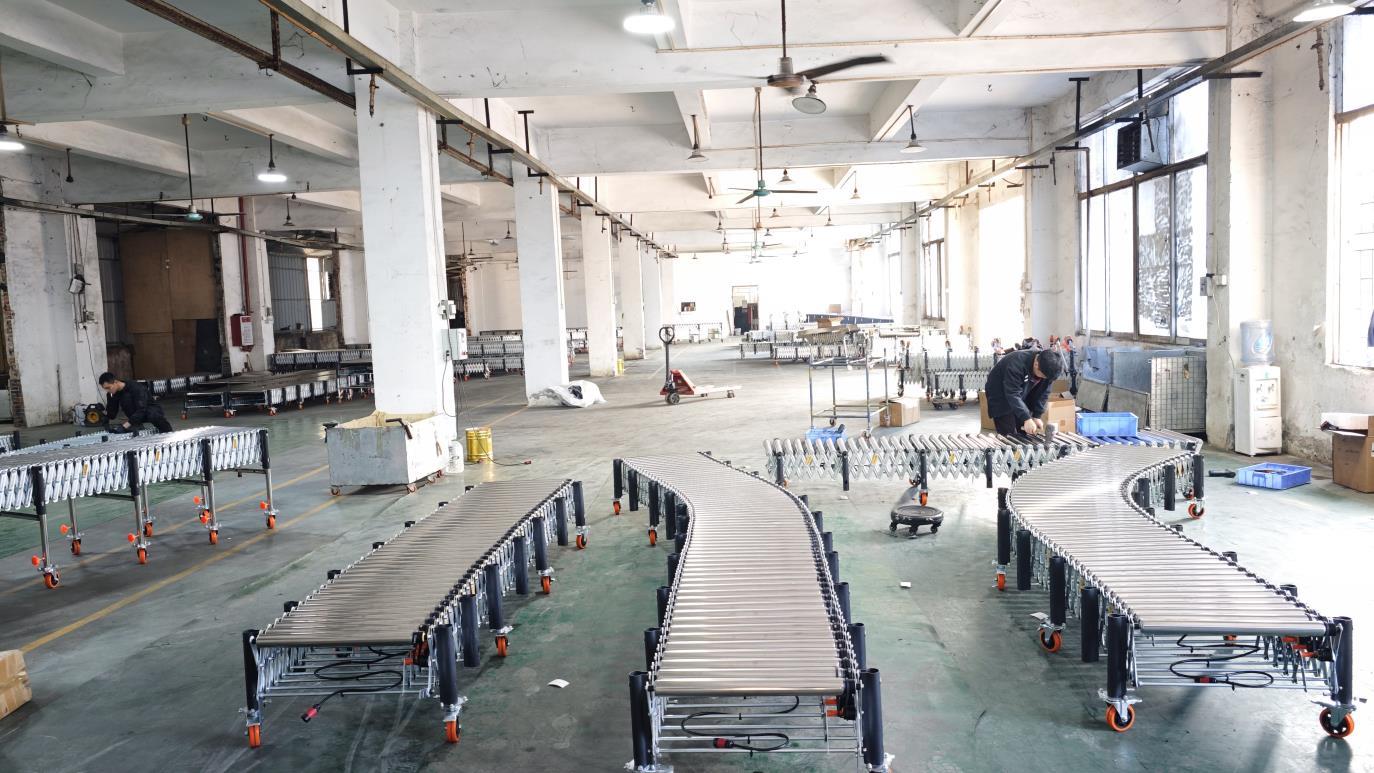
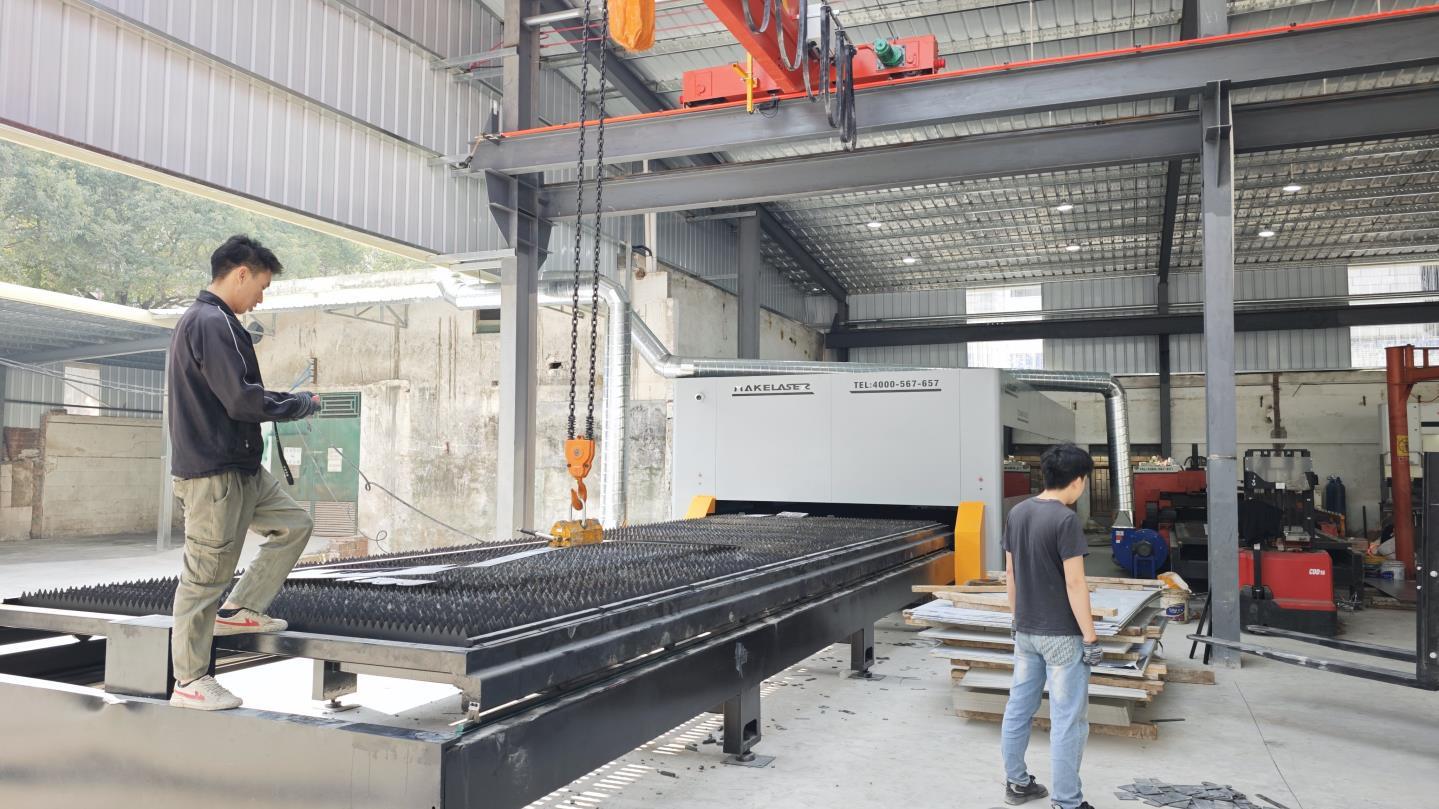
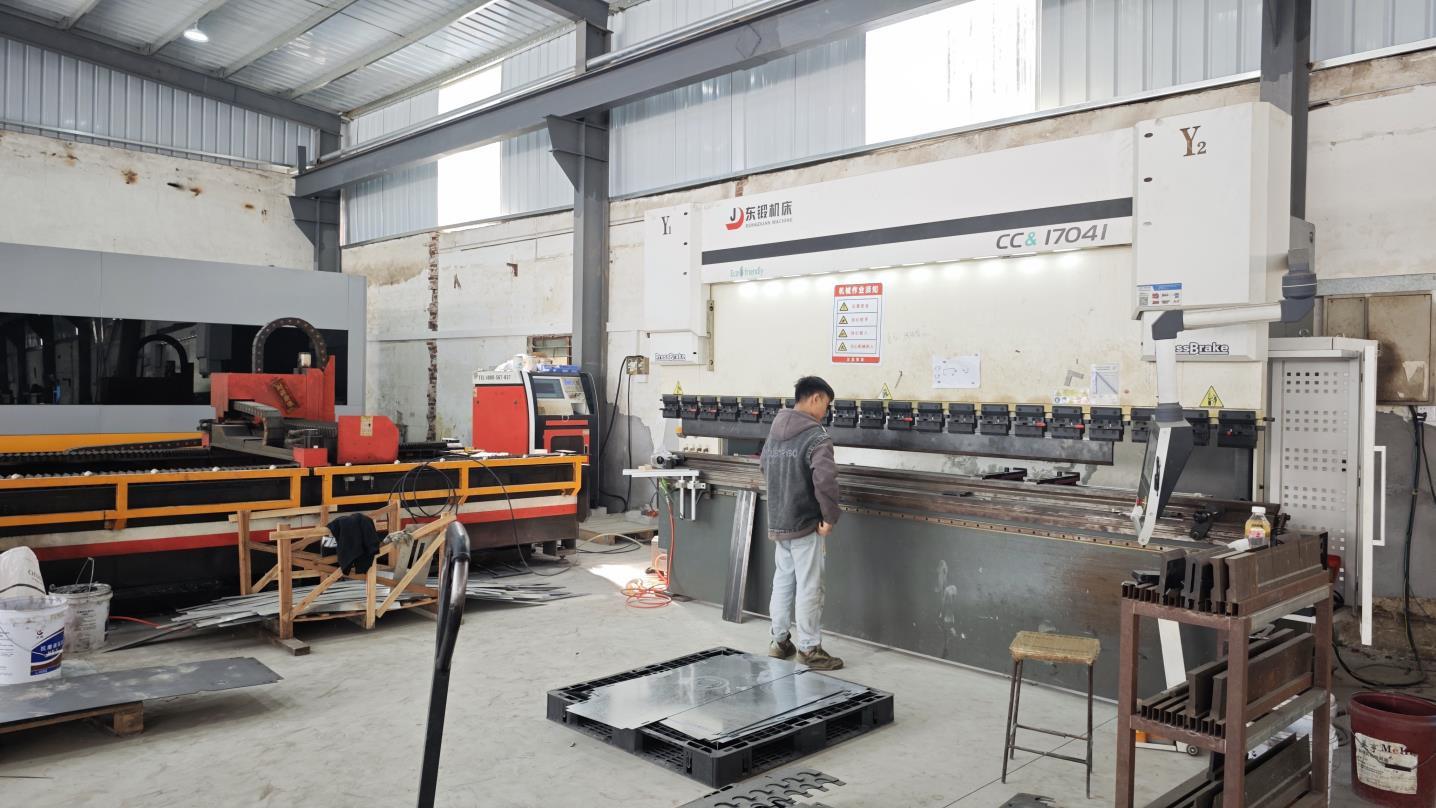
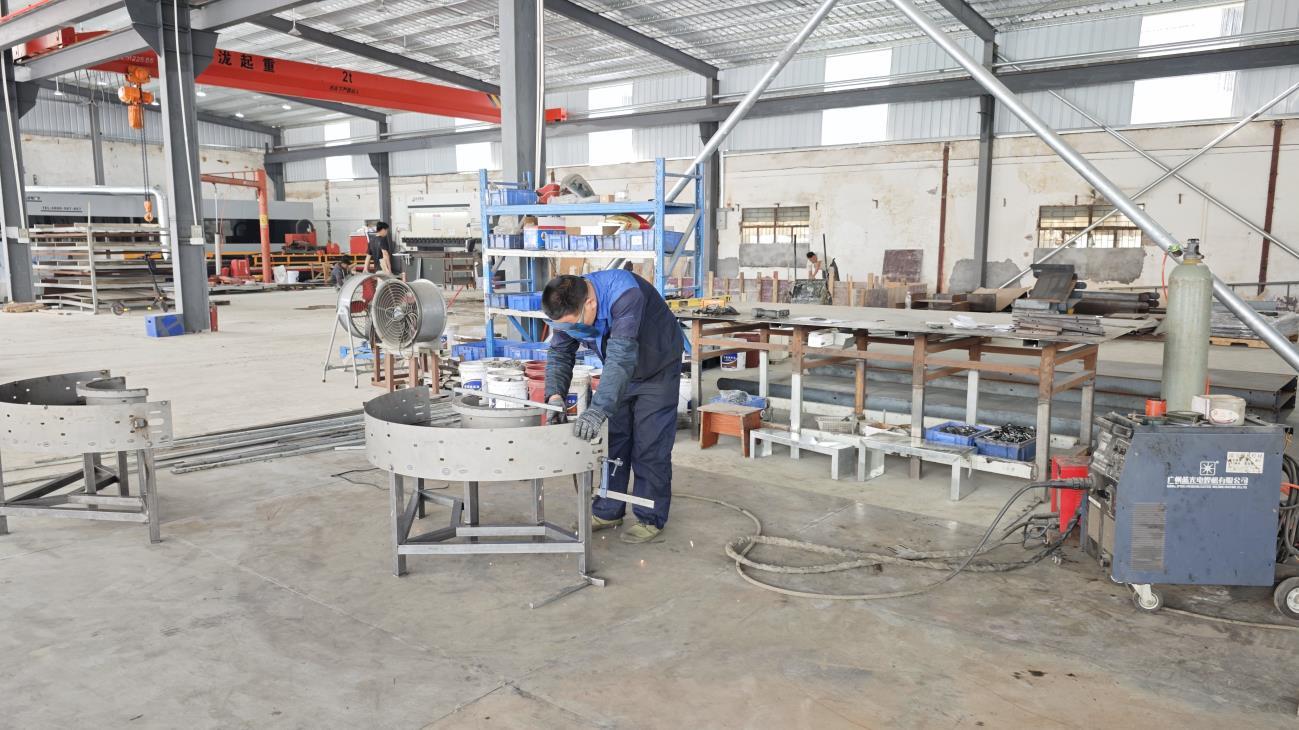
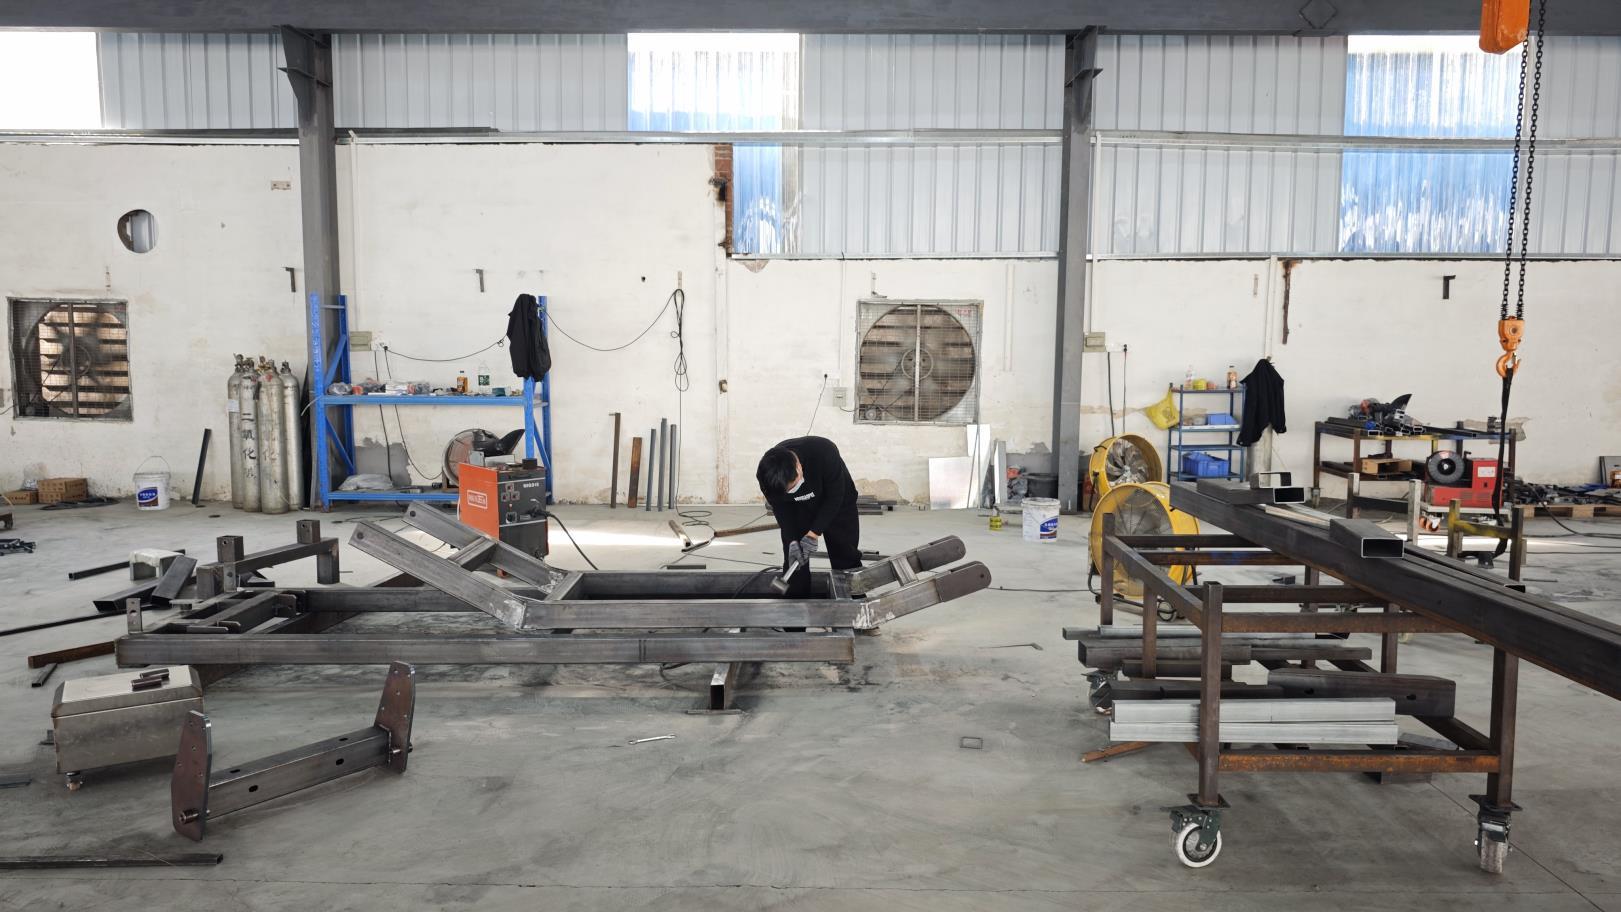
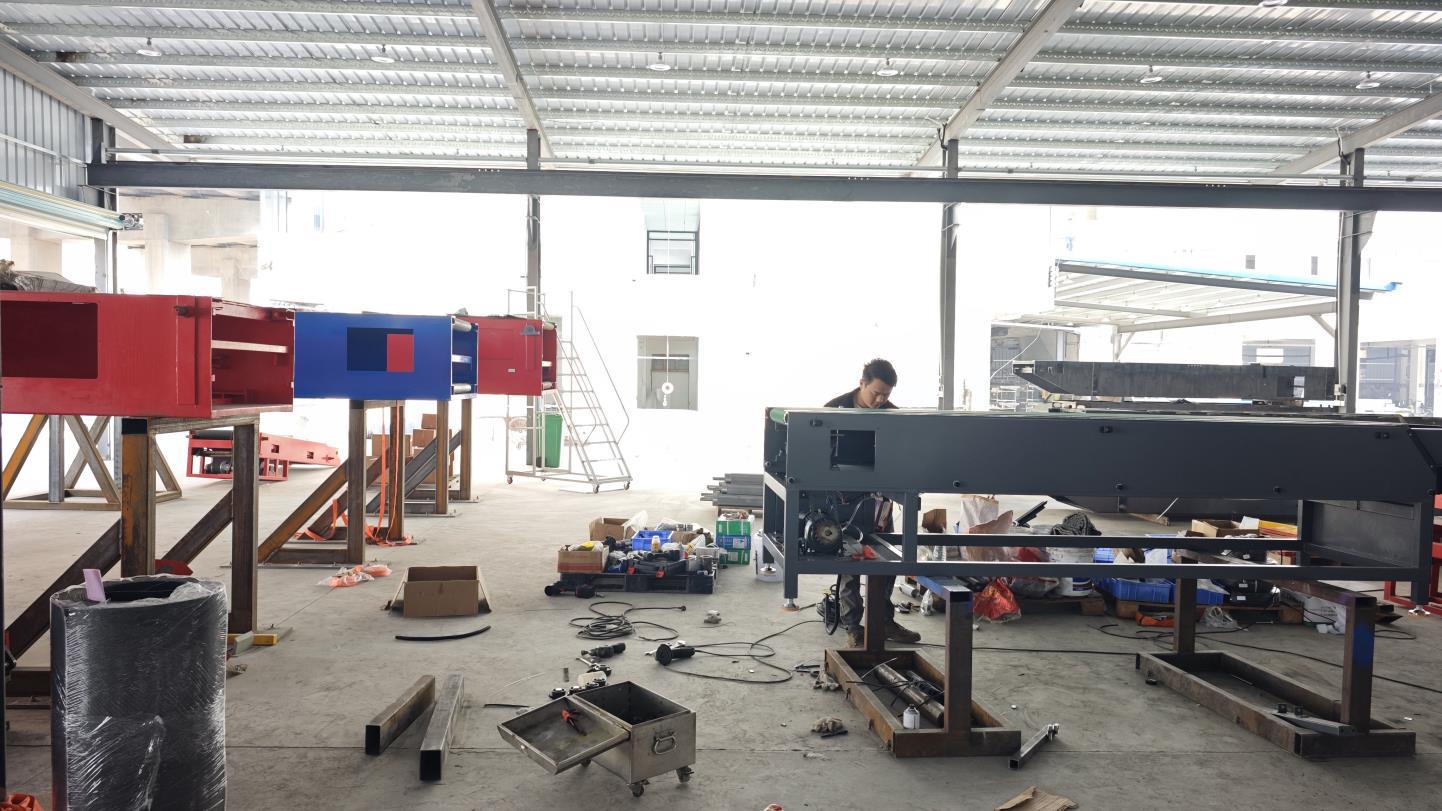
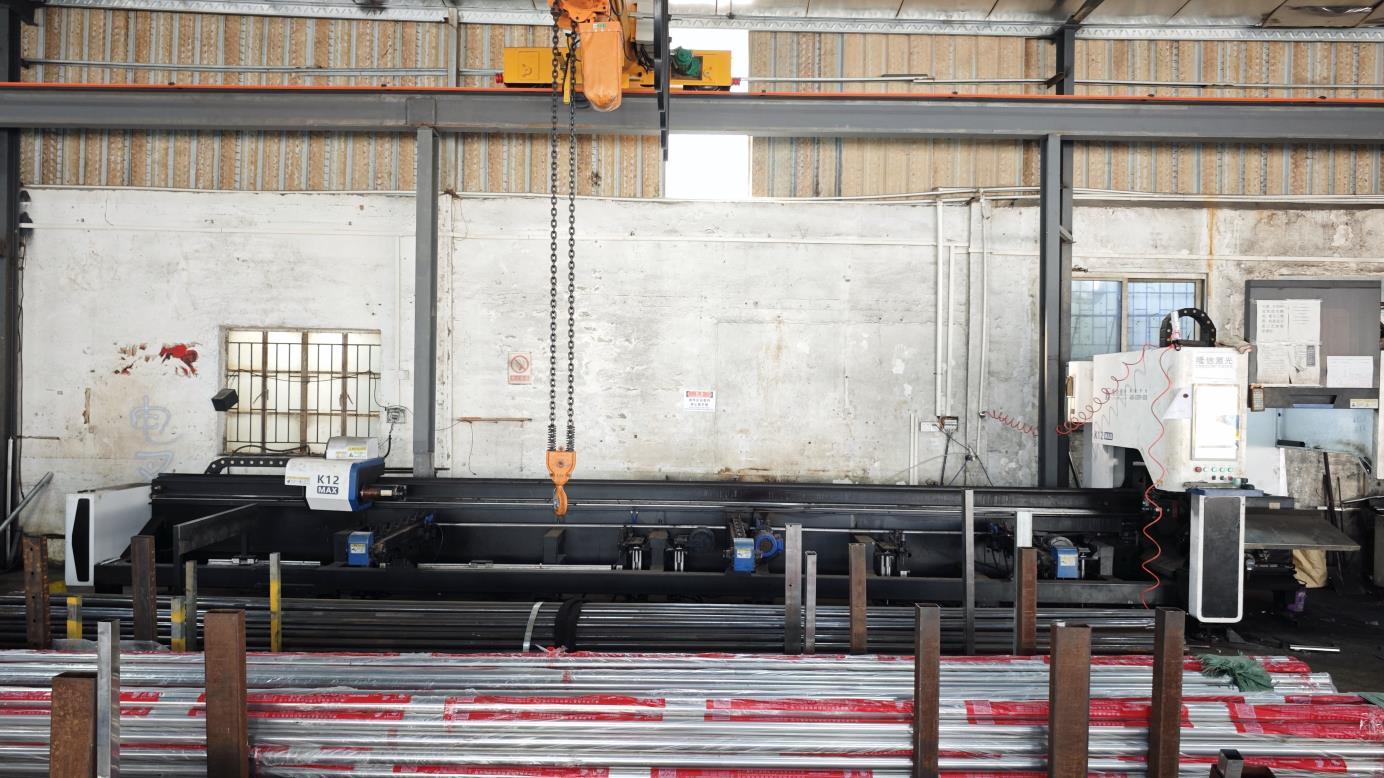
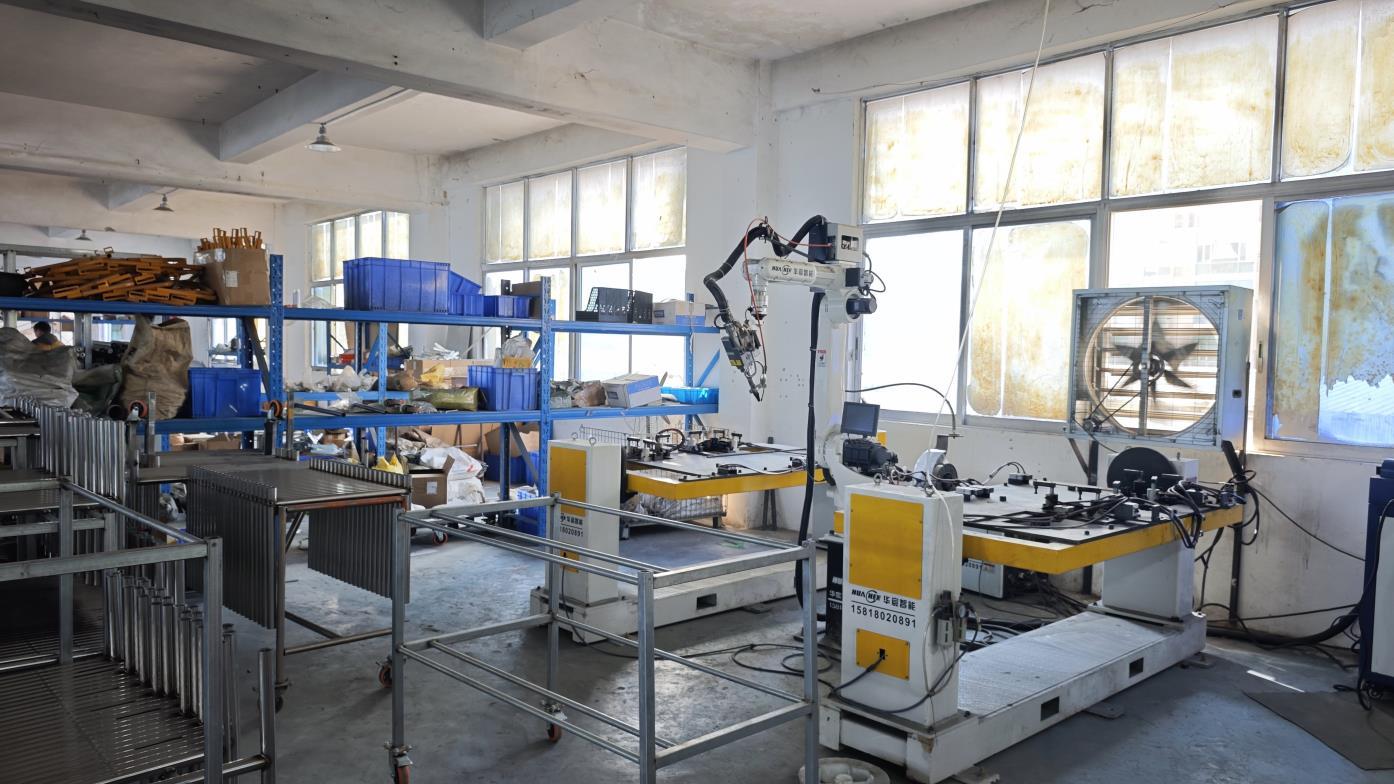
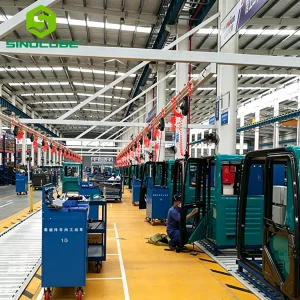
Our state-of-the-art production facilities utilize advanced CNC machinery, automated robotic welding, and stringent quality control protocols to manufacture world-class industrial conveyor systems.
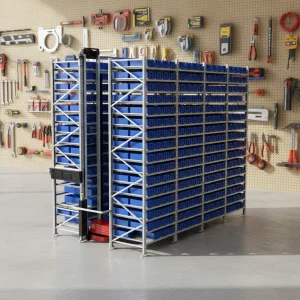
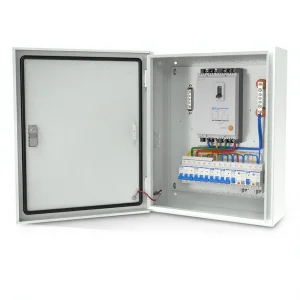
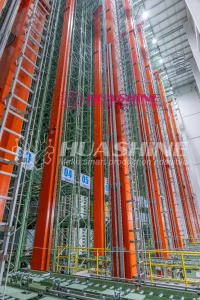
Discover our complementary hardware and software integration products designed to complete your smart warehouse infrastructure.
Expert answers regarding our CE certified industrial conveyors, global shipping compliance, and system integration capabilities.
All our industrial conveyors and automated logistics equipment are fully CE certified, complying with strict European safety, health, and environmental protection requirements. We also adhere to ISO9001 quality management standards to ensure seamless global export and regulatory compliance.
Our conveyor systems feature advanced PLC controllers and open-architecture WCS (Warehouse Control System) software interfaces. This allows effortless integration with major ERP and WMS platforms (including SAP, Oracle, and custom solutions) for real-time item tracking and automated routing.
Yes. We provide end-to-end custom engineering services—from initial site consultation and 3D simulation layout design to precision manufacturing, on-site installation, and lifelong technical support tailored to your unique floor space and throughput targets.
 RAB Logistics